
金属部品向けウェット塗装サービス
SR MFGは、カスタム金属部品、筐体、パネル、ブラケット、製作アセンブリ向けにウェットスプレー塗装サービスを提供しています。色合わせ、膜厚管理、機能領域のマスキング、検査記録をサポートし、外観、耐食性、組立信頼性のバランスを実現します。.
色合わせ
RAL、Pantone、または承認済みの現物サンプルに基づく色合わせ。.
機能領域のマスキング
ねじ山、嵌合面、接地ポイント、接触領域のマスキング。.
検査サポート
外観、膜厚、密着性、梱包品質の検査サポート。.
24時間以内にカスタム見積もりを取得
図面をアップロードしてエンジニアリングレビューを受けてください。.
金属スプレー塗装とは?
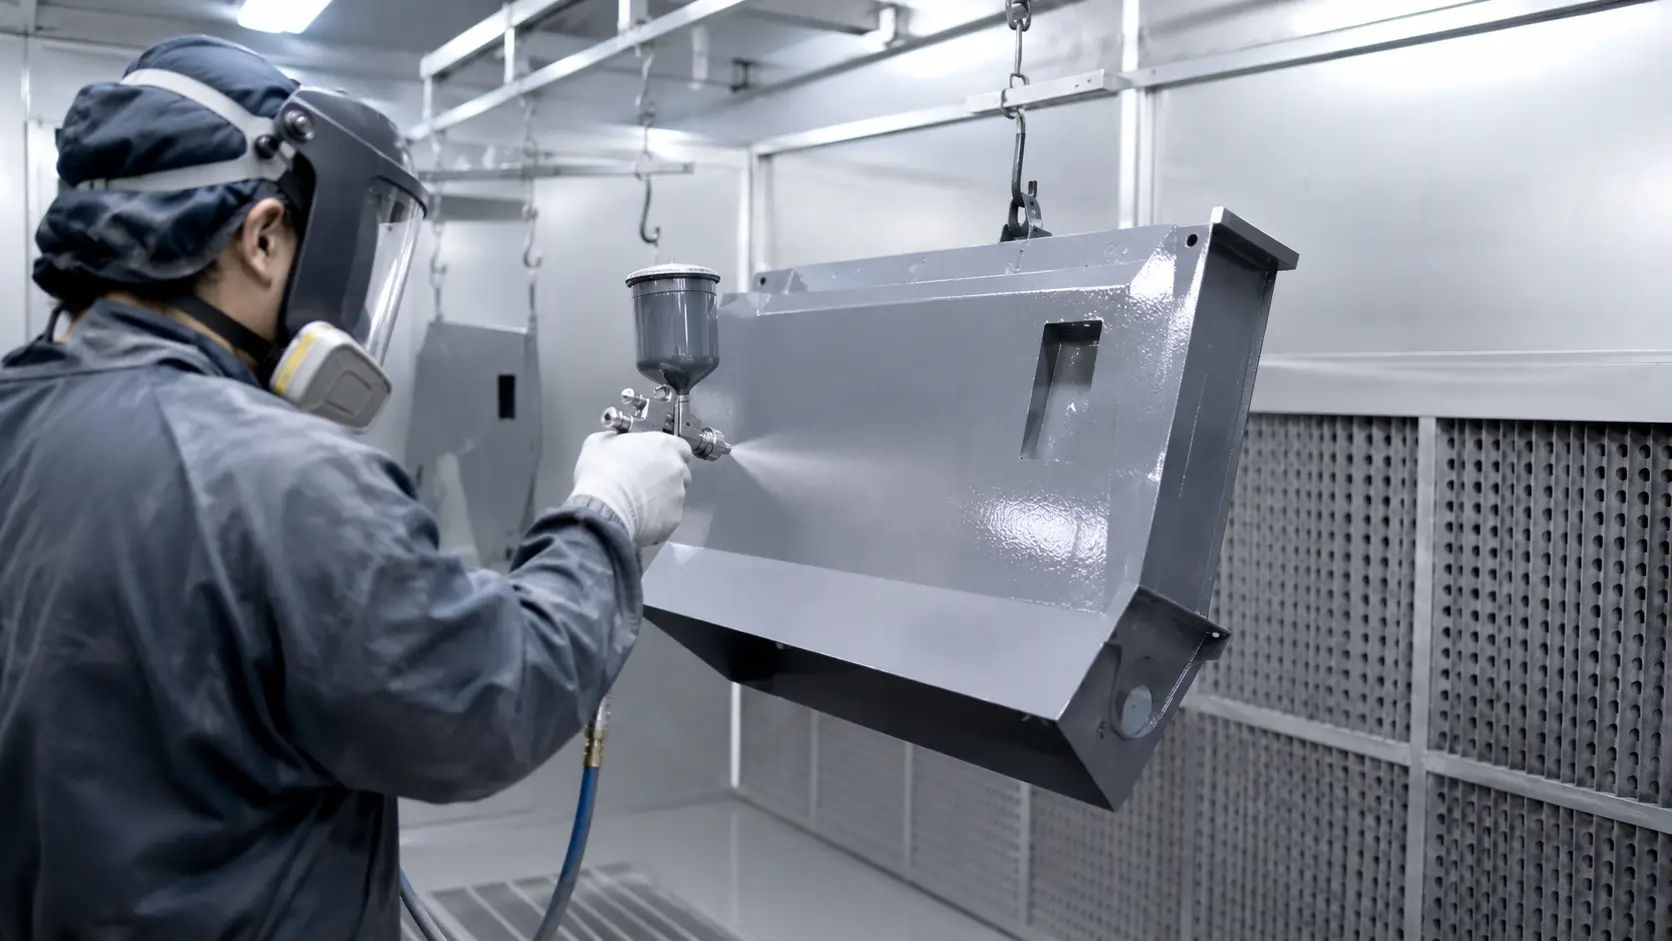
金属スプレー塗装は、スプレー設備を用いて金属部品に液体塗料を塗布するウェットコーティングプロセスです。粉体塗装と比較して、ウェット塗装はカスタムカラー、小ロットプロジェクト、大型部品、タッチアップ作業、プライマーやトップコート、特殊表面効果を必要とするコーティングシステムにおいて、より高い柔軟性を提供します。.
ウェット塗装が選ばれる理由
ウェット塗装はプライマー、中塗り、トップコートなどの多層システムに対応し、仕上がり管理と耐久性において greater な柔軟性を提供します。.
複雑な部品、試作品、小批量生産、大型部品、または粉体塗装が最適でないアセンブリに ideal です。.
一般的な用途
設備
筐体
機械
カバー
ブラケット&
フレーム
カスタム塗装
パネル
柔軟な色・仕上げオプション
ブランドやデザインに合わせた幅広いカスタムカラーと光沢レベル。.
プライマー+トップコートシステム
カスタマイズされた多層コーティングで、耐久性の高い高性能仕上げを実現。.
複雑または小ロット部品に最適
複雑な形状、特殊材料、限られた生産ロットの部品に ideal です。.
当社が一般的に塗装する金属部品
SR MFGは、幅広いカスタム板金部品および製作金属アセンブリにウェットスプレー塗装を提供しています。各プロジェクトは、材料、部品形状、外観グレード、マスキング要件、コーティングシステム、最終検査基準に基づいて検討されます。.
筐体・ハウジング
電気キャビネット、制御ボックス、通信筐体、サーバーシャーシ、および管理された外観と耐食性が求められるカスタムハウジング。.
構造・支持部品
ブラケット、取付プレート、キャリア、レール部品、補強材、フレーム、および耐久性と組立適合性が重要な支持部品。.
プレス・成形部品
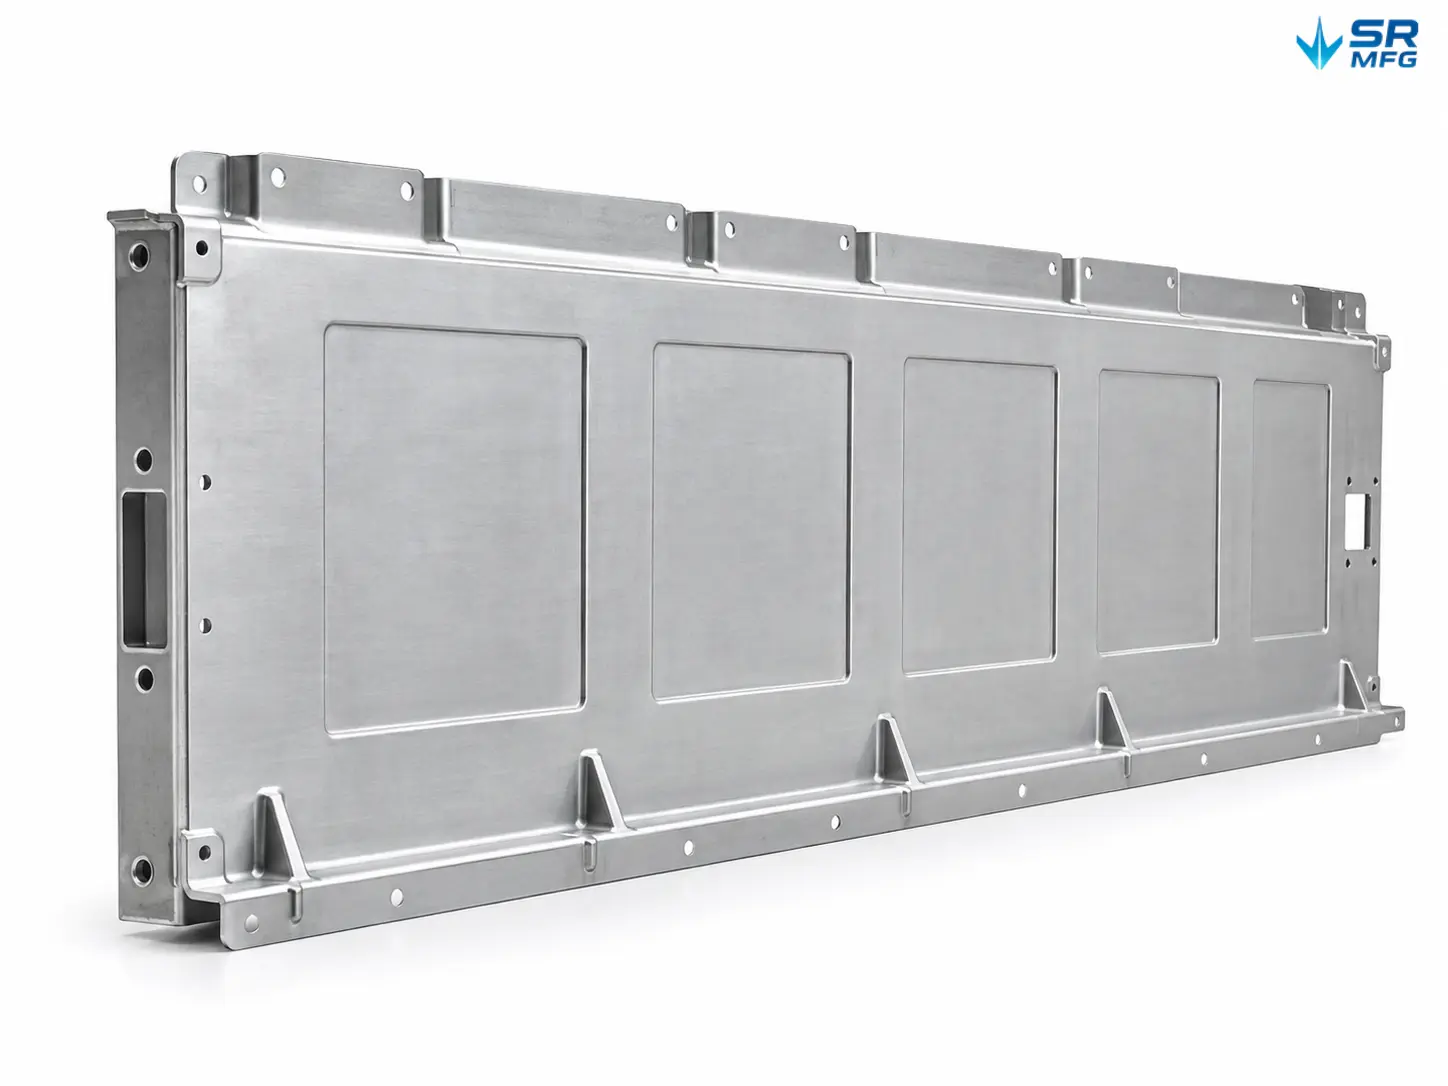
パネル、カバー、トレイ、Uチャンネル、ボックスセクション、および曲げ・プレス後に安定した仕上げ品質が求められる成形部品。.
溶接アセンブリ
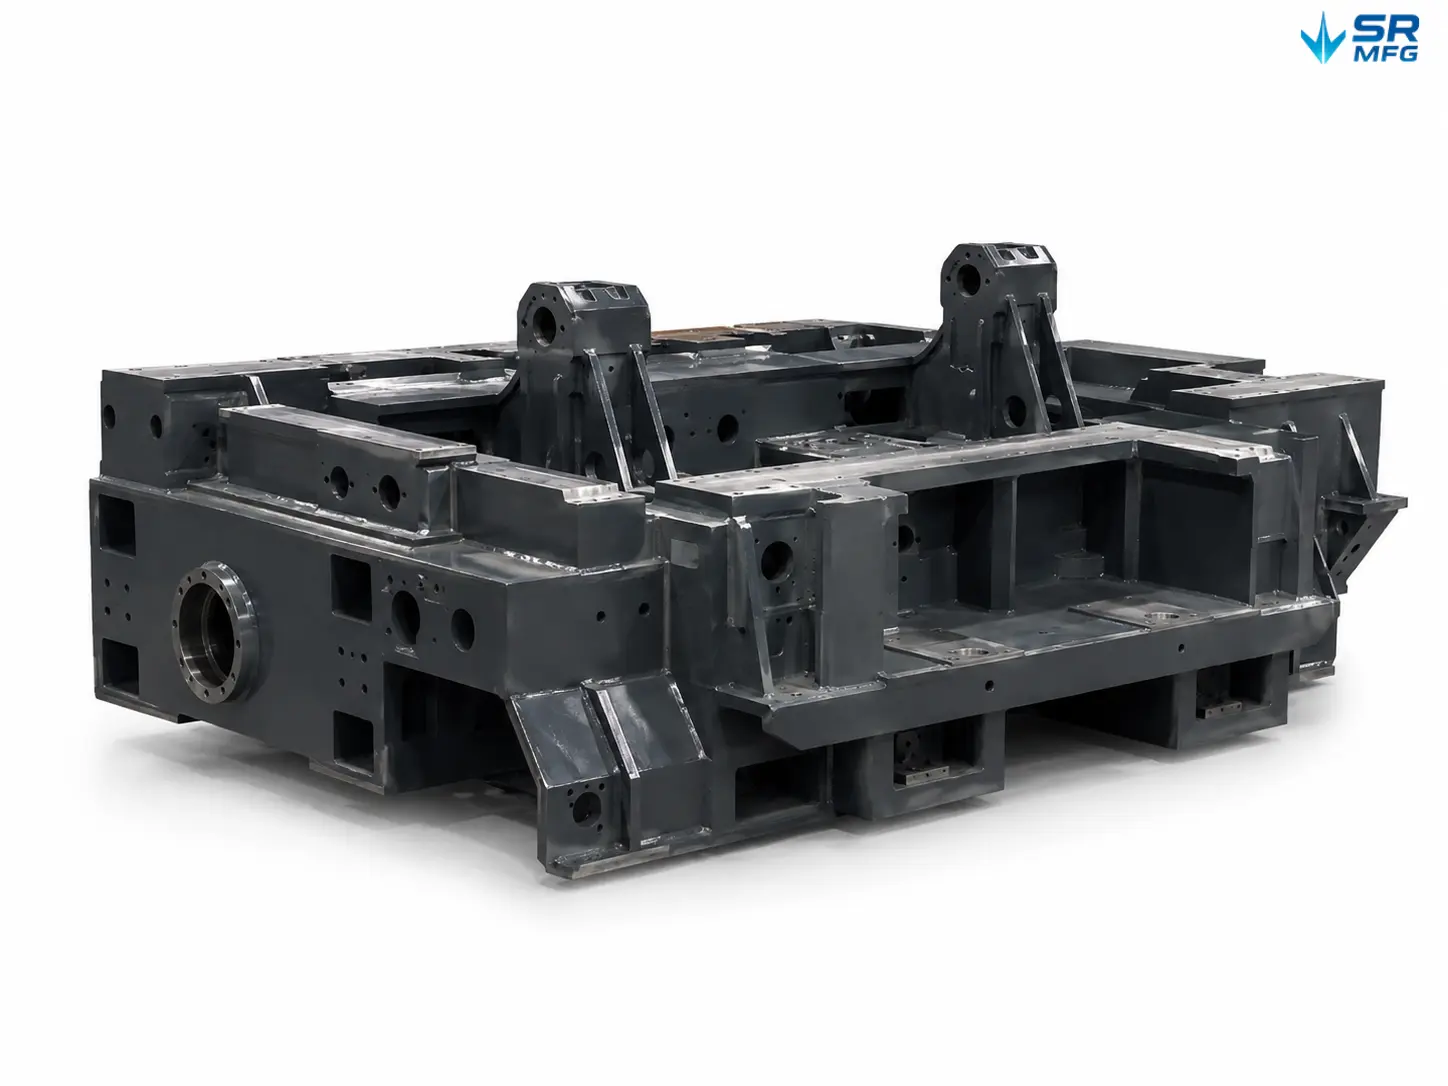
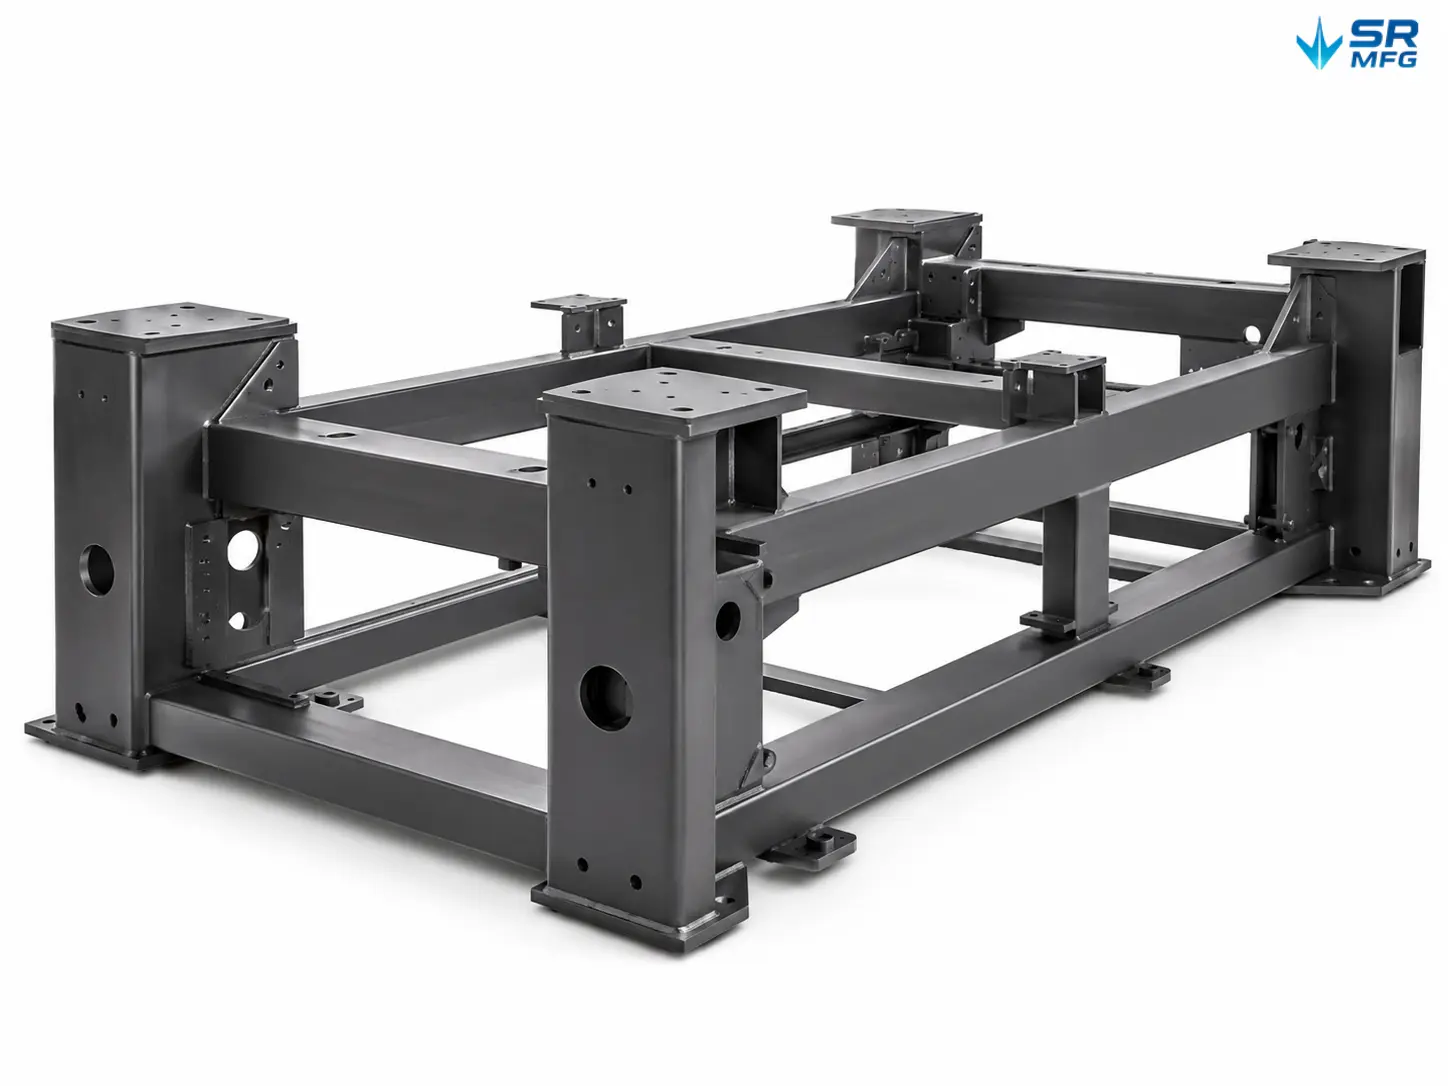
溶接フレーム、溶接筐体、ブラケットアセンブリ、およびシーム処理、マスキング、均一なコーティング被覆が求められる製作構造物。.
外観/クラスA表面
指定された色、光沢、平滑性、承認済みサンプル要件を持つ可視パネルおよび装飾金属部品。.
塗装可能材料と表面処理
当社は一般的に炭素鋼/合金鋼/鋳鉄、アルミニウムおよびアルミニウム合金、ステンレス鋼、亜鉛めっき鋼、およびご要望に応じて銅および銅合金にスプレー塗装を行います。各基材は独自の表面状態とコーティングリスクを持つため、前処理方法をそれに合わせて適合させる必要があります。.
以下は、材料別の塗装および表面処理に関するSR MFGの実用的なプロジェクトベースの推奨事項です。その他の材料や特別な要件がある場合は、お問い合わせください。お客様の用途に最適なプロセスを評価いたします。.
当社が一般的に塗装する材料
金属スプレー塗装の一般的な材料には、炭素鋼、亜鉛めっき鋼、アルミニウム合金、ステンレス鋼があります。最良の結果を得るには、表面処理方法、プライマー選定、塗料タイプ、コーティング膜厚、硬化条件を生産前に併せて検討する必要があります。.
炭素鋼
亜鉛メッキ鋼板
アルミニウム合金
ステンレス鋼
特殊コーティング鋼
炭素鋼
一般的な鋼種: SPCC / DC01 / ASTM A1008
一般的な課題: 裸の冷間圧延鋼は腐食リスクが高い。防錆油、指紋、切削油、微細な表面汚染は塗料密着性を低下させ、フィッシュアイ、クレーター、不均一な外観を引き起こす可能性がある。.
SR MFGの前処理アプローチ:
洗浄・脱脂: 塗装前に圧延油、防錆油、指紋、切削油、取り扱い時の汚染を除去する。.
除錆・表面調整: 酸化、傷、保管痕がある場合、軽度の機械的処理または微細研磨を使用できる。.
化成処理および/またはプライマー: 腐食目標に基づいてリン酸塩、シラン、セラミック化成処理オプションを選択できる。屋外または高湿度用途には防食プライマーを推奨。.
主要管理項目: 表面清浄度、乾燥品質、塗装ウィンドウタイム、プライマー適合性、塗装前のフラッシュラスト防止。.
一般的な鋼種: Q235B / SS400 / ASTM A36 / S235JR
一般的な課題: ミルスケール、錆、溶接スパッタ、粗い表面性状は塗膜密着性を低下させ、目に見える塗装欠陥を生じさせる可能性がある。表面処理は冷間圧延鋼よりも重要である。.
SR MFGの前処理アプローチ:
洗浄・脱脂: ブラスト処理または機械的前処理の前に、切削油、機械油、指紋、加工時の汚染を除去する。.
除錆・表面調整: ブラスト、研削、または機械的デスケーリングを使用して、浮きミルスケールと錆を除去し、プライマー密着に適した表面性状を形成する。.
化成処理および/またはプライマー: 塗装システムに応じてリン酸亜鉛、リン酸鉄、シラン、セラミック前処理を使用できる。構造部品または屋外部品には防食プライマーを推奨。.
主要管理項目: ミルスケール除去レベル、表面性状の均一性、溶接部の清浄度、エッジカバレッジ、プライマー塗布前の塗装ウィンドウタイム。.
一般的な鋼種: SPHC-P / DD11 / ASTM A1011 P&O
一般的な課題: 表面は通常の熱間圧延鋼よりも清浄であるが、塗装前に油膜を完全に除去する必要がある。残留油は密着不良、フィッシュアイ、プライマーの濡れ不良を引き起こす可能性がある。.
SR MFGの前処理アプローチ:
洗浄・脱脂: 塗装前に酸洗油、防錆油、切削油、指紋を除去する。.
除錆・表面調整: 通常は熱間圧延鋼よりも軽度で済む。エッジ、溶接部、または酸化した保管材には研磨や機械的前処理を使用することがある。.
化成処理および/またはプライマー: リン酸塩、シラン、セラミック化成処理は塗料密着性と耐食性を向上させることができる。プライマーの選択は屋内または屋外用途に依存する。.
主要管理項目: 油分除去、水切れ良好な表面状態、エッジ清浄度、乾燥品質、前処理から塗装までの時間。.
一般的な鋼種: Q355 / S355 / ASTM A572
一般的な課題: 炭素鋼と同様の腐食リスクがあるが、構造部品は溶接部、厚いエッジ、荷重支持面が多く、より優れたエッジ保護とプライマーカバレッジが必要である。.
SR MFGの前処理アプローチ:
洗浄・脱脂: 機械油、切削油、溶接残留物、指紋、一般的な工場汚染を除去する。.
除錆・表面調整: 溶接構造または重荷重構造にはブラスト処理または機械的前処理を推奨し、プライマー密着性と塗膜耐久性を向上させる。.
化成処理および/またはプライマー: リン酸塩またはシラン前処理を防食プライマーと併用できる。より高い耐食性が必要な場合はジンクリッチプライマーを選択することがある。.
主要管理項目: 溶接部の清浄化、エッジの面取り、表面性状、プライマー膜厚、再塗装ウィンドウ、穴および切断エッジ周辺の腐食保護。.
亜鉛めっき材料
一般的な鋼種: SGCC / DX51D+Z / ASTM A653
一般的な課題: 不動態化、白錆、油、保管時の汚染が除去されていない場合、亜鉛表面が塗料密着性に影響を与える可能性がある。成形部または切断エッジには追加の保護が必要な場合がある。.
SR MFGの前処理アプローチ:
洗浄・脱脂: 不動態化残渣、保管油、指紋、切削油、表面汚染を除去する。.
除錆・表面調整: 白錆、酸化、密着リスクがある場合、軽度の研磨、スイープブラスト、または機械的前処理を使用することがある。.
化成処理および/またはプライマー: リン酸塩、シラン、セラミック化成処理などの亜鉛対応前処理を使用できる。腐食性能が重要な場合、亜鉛めっき対応プライマーを推奨。.
主要管理項目: 亜鉛層を損傷する過度に激しいブラストを避ける。密着性、白錆除去、切断エッジ保護、プライマーと亜鉛めっき表面の適合性を管理する。.
一般的な鋼種: SECC / DX51D+ZE
一般的な課題: 亜鉛皮膜は溶融亜鉛めっき鋼よりも薄く均一であるが、油、指紋、表面不動態化は依然として塗料密着性を低下させる可能性がある。.
SR MFGの前処理アプローチ:
洗浄・脱脂: スプレー塗装前にプレス油、指紋、切削油、軽度の表面汚染を除去する。.
除錆・表面調整: 通常は軽度の機械的前処理のみ。不要な亜鉛皮膜損傷を防ぐため、過度の研磨は避けるべきである。.
化成処理および/またはプライマー: リン酸塩、シラン、セラミック前処理を選択できる。塗装筐体、キャビネット、屋内/屋外制御盤にはプライマーを推奨。.
主要管理項目: 塗膜密着性、表面清浄度、亜鉛層保護、塗料の濡れ性、乾燥または焼付後の安定した外観。.
一般的な鋼種: DX51D+ZF / ASTM A653 A40 / A60
一般的な課題: 亜鉛-鉄表面は一般に塗装性が良好であるが、パウダリング、成形残渣、緩い表面粒子が外観と密着性に影響を与える可能性がある。.
SR MFGの前処理アプローチ:
洗浄・脱脂: 塗装前に成形油、粉塵、緩い粒子、切削油、指紋を除去する。.
除錆・表面調整: 成形エッジ、溶接部、または汚染領域には軽度のブラッシング、拭き取り、または機械的清浄を使用することがある。.
Conversion coating and/or primer: Phosphate or silane pretreatment can support better adhesion; primer is selected based on corrosion and appearance requirements.
Key controls: Surface powder removal, paint adhesion, formed-edge coverage, weld-area cleaning, and primer compatibility.
アルミニウム合金
Common Grades: 5052-H32 / 5052-H34
Common challenges: Aluminum forms a natural oxide layer and can show scratches, fingerprints, and handling marks after painting. Poor pretreatment may cause adhesion loss or corrosion under coating.
SR MFGの前処理アプローチ:
Cleaning & degreasing: Removes machining oil, cutting fluids, fingerprints, polishing residue, and shop contamination.
Rust removal & surface profiling: Light sanding, scuffing, or non-ferrous surface preparation can be used to improve mechanical adhesion without damaging the part surface.
Conversion coating and/or primer: Non-chrome or chrome-free conversion coating, silane, zirconium/ceramic pretreatment, or aluminum-compatible primer can be selected based on corrosion targets.
Key controls: Oxide removal/activation, surface cleanliness, pretreatment chemistry compatibility, primer adhesion, and color consistency after painting.
Common Grades: 6061-T6 / 6061-T651
Common challenges: Machined and formed 6061 surfaces may show tool marks, oxide film, and batch-to-batch surface variation. Paint appearance can be affected by sanding marks and surface texture.
SR MFGの前処理アプローチ:
Cleaning & degreasing: Removes machining coolant, cutting oil, fingerprints, and abrasive residue before painting.
Rust removal & surface profiling: Light sanding, scuffing, or controlled blasting can be used to create a uniform surface for primer adhesion.
Conversion coating and/or primer: Aluminum conversion coating or chrome-free pretreatment can be paired with epoxy or polyurethane primer for improved adhesion and corrosion resistance.
Key controls: Surface profile uniformity, oxide control, primer compatibility, masking accuracy, and protection of threaded or machined areas.
Common Grades: 3003-H14 / 3003-H24
Common challenges: Soft aluminum is easy to scratch or dent before painting. Surface marks may remain visible through thin paint films if not prepared properly.
SR MFGの前処理アプローチ:
Cleaning & degreasing: Removes rolling oil, handling marks, fingerprints, and forming lubricants.
Rust removal & surface profiling: Light sanding or scuffing can improve paint adhesion and help reduce visible surface defects.
Conversion coating and/or primer: Aluminum-compatible conversion coating or primer can be used depending on indoor, outdoor, or decorative requirements.
Key controls: Handling protection, scratch prevention, surface uniformity, primer wetting, and clean drying before painting.
Common Grades: 5754-H22 / 5754-H111
Common challenges: Good corrosion resistance, but formed aluminum panels can still have oxide film, forming lubricant, and visible surface marks that affect paint appearance.
SR MFGの前処理アプローチ:
Cleaning & degreasing: Removes forming oil, fingerprints, cutting fluids, and storage contamination.
Rust removal & surface profiling: Light mechanical preparation or non-ferrous surface conditioning can improve adhesion and appearance.
Conversion coating and/or primer: Chrome-free conversion coating, silane, ceramic pretreatment, or aluminum-compatible primer can be selected for outdoor or transportation applications.
Key controls: Pretreatment uniformity, adhesion after forming, edge coverage, surface appearance, and coating performance in outdoor environments.
ステンレス鋼
Common Grades: 304 / 304L
Common challenges: Stainless steel has a passive surface that can make paint adhesion more difficult than carbon steel. Fingerprints, polishing compound, welding discoloration, and oil can compromise coating adhesion.
SR MFGの前処理アプローチ:
Cleaning & degreasing: Removes fingerprints, polishing paste, cutting fluids, adhesive residue, and welding-related contamination.
Rust removal & surface profiling: Light abrasive preparation, scuffing, or blasting with stainless-compatible media can improve mechanical adhesion.
Conversion coating and/or primer: Stainless-compatible primer is usually more important than traditional steel phosphating; epoxy primer or adhesion-promoting primer may be selected.
Key controls: Surface roughness, clean passive surface, primer adhesion, weld discoloration removal, and avoiding cross-contamination from carbon steel tools.
Common Grades: 316 / 316L
Common challenges: 316 stainless steel is highly corrosion resistant, but this also means paint adhesion can be more demanding. Marine or chemical applications require careful primer selection.
SR MFGの前処理アプローチ:
Cleaning & degreasing: Removes oil, fingerprints, polishing residue, cutting fluids, and chloride contamination before painting.
Rust removal & surface profiling: Controlled scuffing or blasting can be used to create adhesion profile without damaging the stainless surface.
Conversion coating and/or primer: Adhesion-promoting primer, epoxy primer, or high-performance coating system is recommended for marine, outdoor, or chemical environments.
Key controls: Chloride contamination control, surface profile, primer compatibility, recoat window, and long-term adhesion under corrosive exposure.
Common Grades: 201 / 201J1 / 201J2
Common challenges: Lower corrosion resistance than 304, and surface quality can vary by batch. Painted 201 parts need reliable pretreatment to reduce corrosion risk at edges, scratches, and welds.
SR MFGの前処理アプローチ:
Cleaning & degreasing: Removes polishing compound, fingerprints, cutting fluids, and fabrication contamination.
Rust removal & surface profiling: Light sanding or scuffing can improve adhesion; weld discoloration and contaminated areas should be cleaned before primer.
Conversion coating and/or primer: Stainless-compatible primer or epoxy primer is recommended when corrosion protection is needed.
Key controls: Edge protection, weld cleaning, surface uniformity, primer adhesion, and avoiding use in harsh outdoor environments unless coating system is specified.
Common Grades: 430 / 430BA
Common challenges: 430 stainless steel is often used for decorative and appliance parts, but its lower corrosion resistance and lower formability compared with 304 require better edge and surface protection when painted.
SR MFGの前処理アプローチ:
Cleaning & degreasing: Removes fingerprints, polishing residue, protective film adhesive, and forming oil.
Rust removal & surface profiling: Light scuffing or fine abrasive preparation can improve paint adhesion while maintaining decorative surface quality.
Conversion coating and/or primer: Adhesion-promoting primer or stainless-compatible primer can be used for painted decorative panels and appliance parts.
Key controls: Surface appearance, scratch control, primer wetting, edge coverage, and prevention of contamination from carbon steel particles.
注記: Recommended paint system and coating specifications depend on material type, surface condition, part geometry, application environment, and end-use requirements. Surface preparation, primer selection, paint type, and curing process should be evaluated together for optimal adhesion and finish quality. Please share drawings and technical specifications for engineering review before production.
SR MFG Spray Painting Process Flow
SR MFG Metal Part Spray Painting Process Flow
Requirement & Finish Review
Confirm drawings, color, gloss, masking areas, and inspection standards.
Incoming Inspection & Surface Prep
Check part condition; complete sanding, deburring, or repair if needed.
Cleaning & Pretreatment
Remove oil, dust, and contaminants; apply suitable pretreatment.
Masking & Fixturing
Protect threads, mating surfaces, grounding points, and no-paint zones.
Primer / Topcoat Application
Apply primer, intermediate coat, or topcoat based on the coating system.
Drying / Curing & Cooling
Dry or bake parts per paint-system requirements, then cool carefully.
Final Inspection & Packing
Check appearance, color, film build, masking quality, and packing condition.
Common Paint Colors & Finish Options
SR MFG supports spray painting finishes for custom sheet metal parts based on project requirements, including color, gloss level, surface texture, coating system, and approved physical samples. The color samples below are for reference only and should be confirmed by RAL code, Pantone code, customer sample, or signed production sample before mass production.
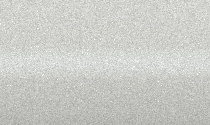
Gloss White
Clean and bright finish for electrical enclosures, control boxes, medical equipment panels, and visible sheet metal housings.
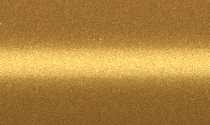
Metallic Gold
Decorative metallic finish for display parts, branded components, covers, and custom appearance projects.
Matte Black
Low-reflection finish for industrial equipment, machine covers, brackets, panels, and functional metal parts.
Deep Blue
Brand-color finish commonly used for equipment covers, panels, enclosures, and customer-specific product lines.
Dark Gray
Neutral industrial finish suitable for machinery guards, cabinet shells, structural parts, and general fabricated components.
Silver Gray
Clean technical appearance for control cabinets, instrument housings, panels, and equipment enclosures.
Olive Green
Durable industrial color option for outdoor equipment, utility housings, brackets, and protective covers.
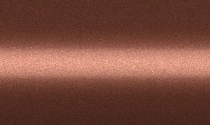
Copper Brown
Warm metallic-style appearance for decorative covers, branded panels, and custom painted metal parts.
Ready to Discuss Your Metal Painting Requirements?
Not sure which paint system is suitable for your project? Contact us with your drawings, material, color, gloss level, service environment, masking requirements, and inspection standards. Our engineering team will review your requirements and recommend a suitable painting solution.
Industries & Metal Spray Painting Applications
SR MFG provides professional metal spray painting services for OEM components used in industrial equipment, cabinets, brackets, frames, enclosures, and structural assemblies. We support both prototype finishing and stable batch production across multiple application sectors.
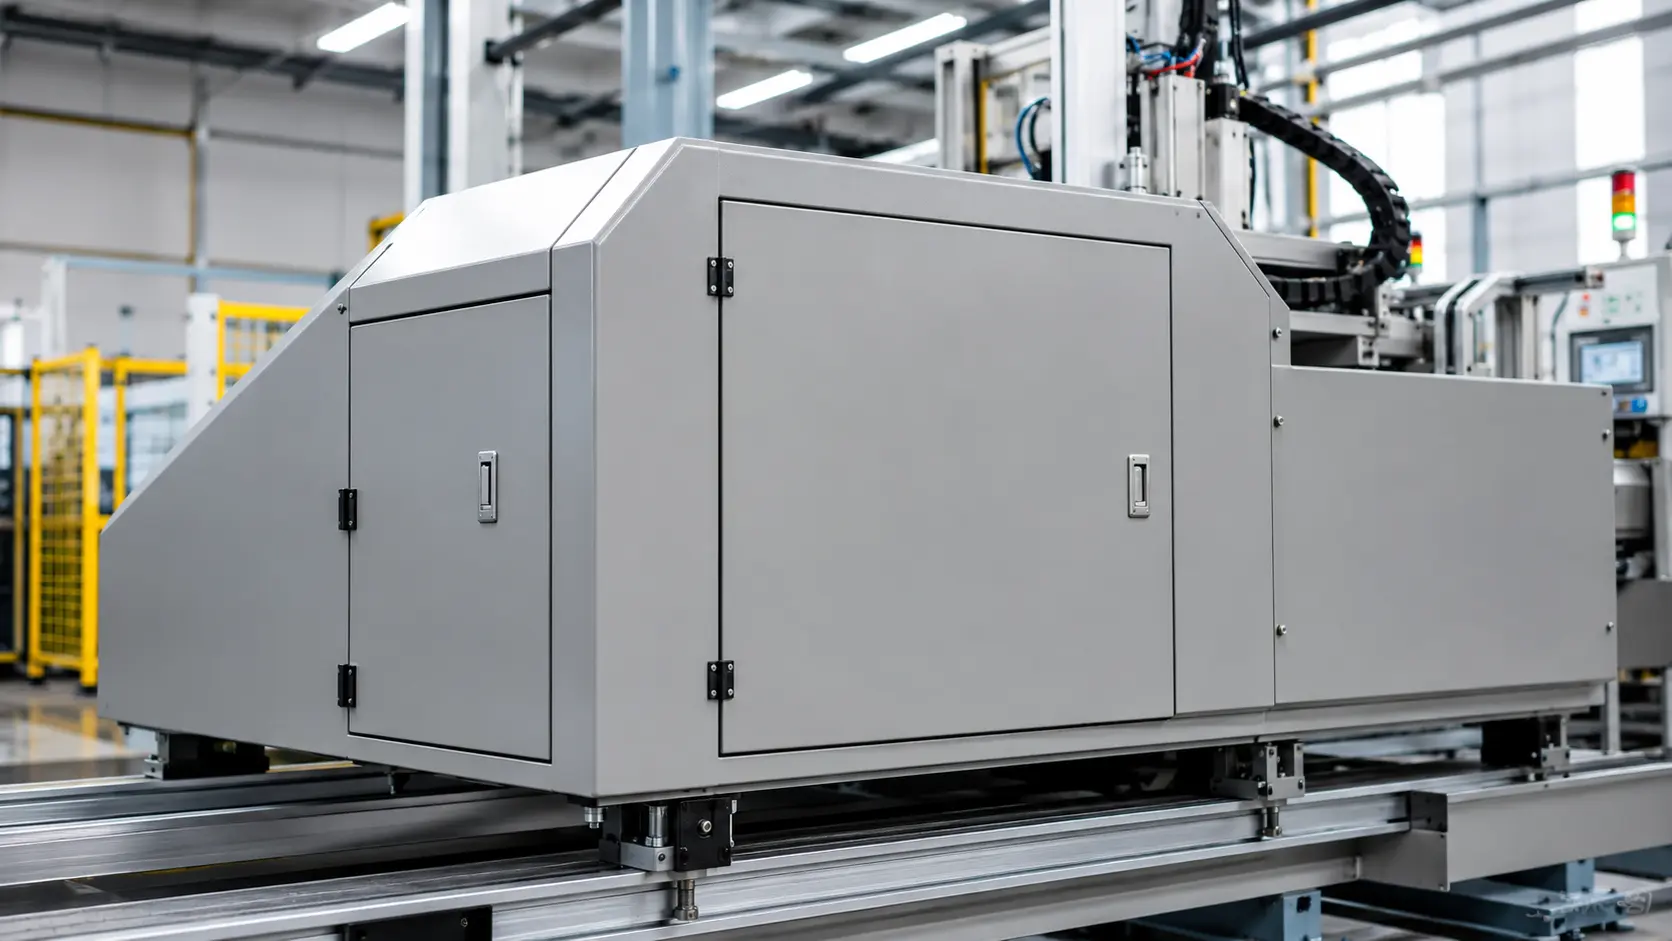
データセンターおよびIT機器
Metal spray painting for data center components, network infrastructure, and IT hardware, delivering smooth, durable finishes with excellent coverage and color consistency.
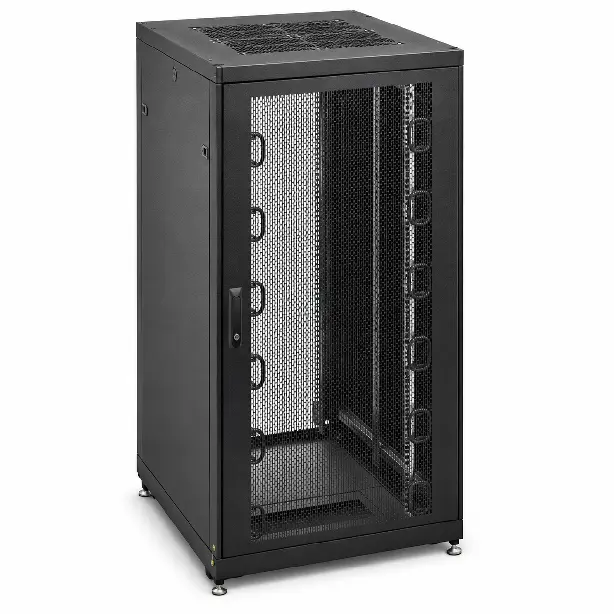
- サーバーラックフレームおよびレール
- ケーブル管理トレイ
- キャビネットパネルおよびドア
- 取付ブラケットおよびプレート
コンシューマーエレクトロニクス
Custom spray painting for consumer electronics housings, internal brackets, display structures, and precision metal assemblies, providing refined surface appearance with scratch and fingerprint resistance.
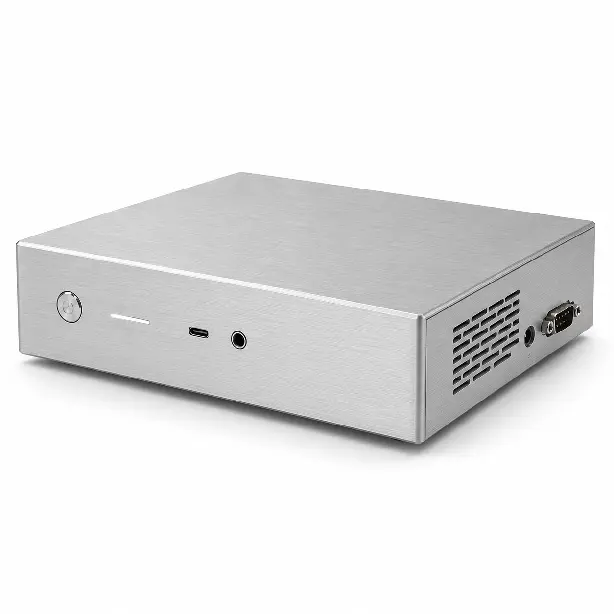
- デバイス筐体&カバー
- 内部支持ブラケット
- ディスプレイ取付構造体
- スピーカー&オーディオ金属部品
- 小型精密成形部品
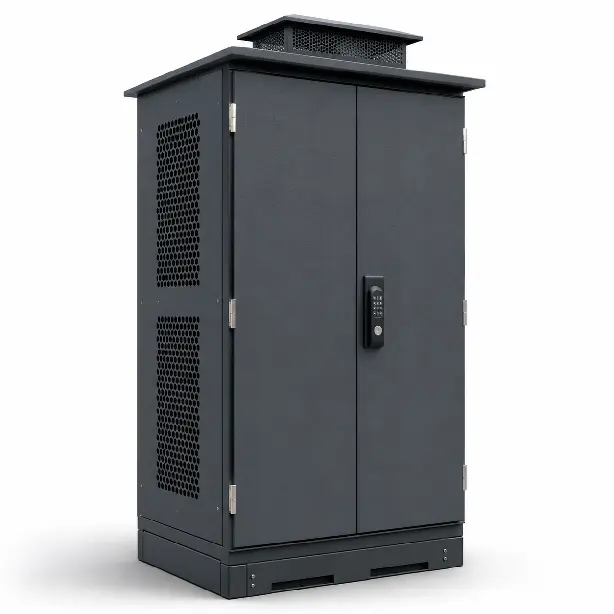
電気設備
Metal spray painting for electrical enclosures, control cabinets, power distribution units, and industrial electrical components, offering strong corrosion resistance and reliable insulation compatibility.
- 電気キャビネット筐体
- 制御ボックスパネル
- 端子取付板
- DINレールブラケット
- 通気・アクセスパネル
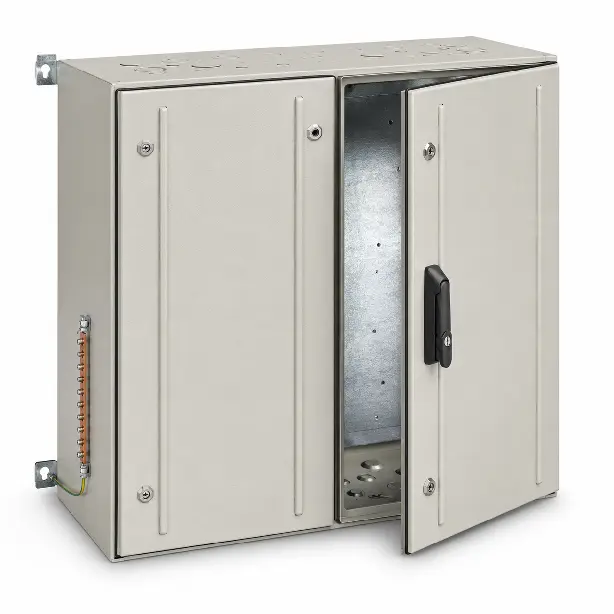
産業機械
Durable spray painted finishes for machinery, automation systems, production equipment, and structural machine assemblies, built to resist chipping, abrasion, and shop-floor wear.
- 機械カバー&ガード
- 設備フレーム
- コンベアブラケット
- センサ取付板
- 保護パネル&シールド
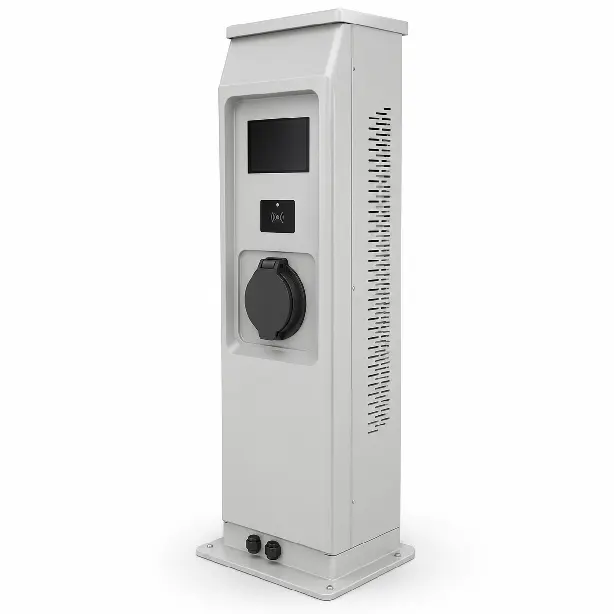
新エネルギーシステム
Metal spray painting solutions for EV charging equipment, battery systems, energy storage cabinets, and power conversion units, delivering long-lasting finishes rated for demanding indoor and outdoor environments.
- バッテリー筐体部品
- 充電ステーションキャビネット
- エネルギー貯蔵キャビネットパネル
- バスバー支持ブラケット
- パワーモジュール筐体
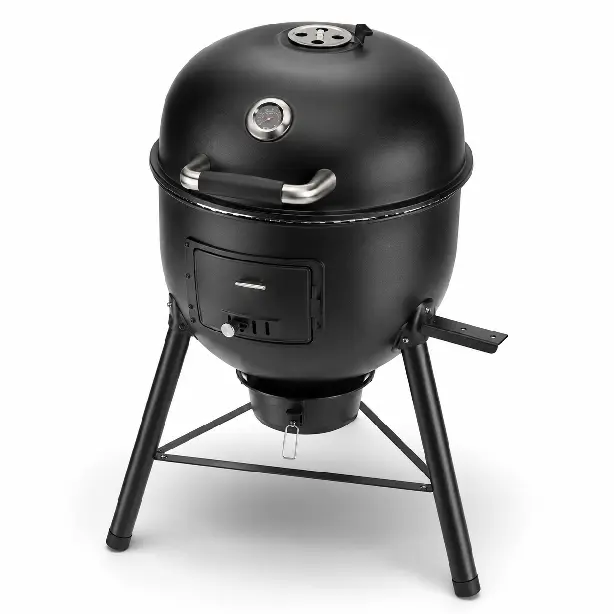
屋外設備
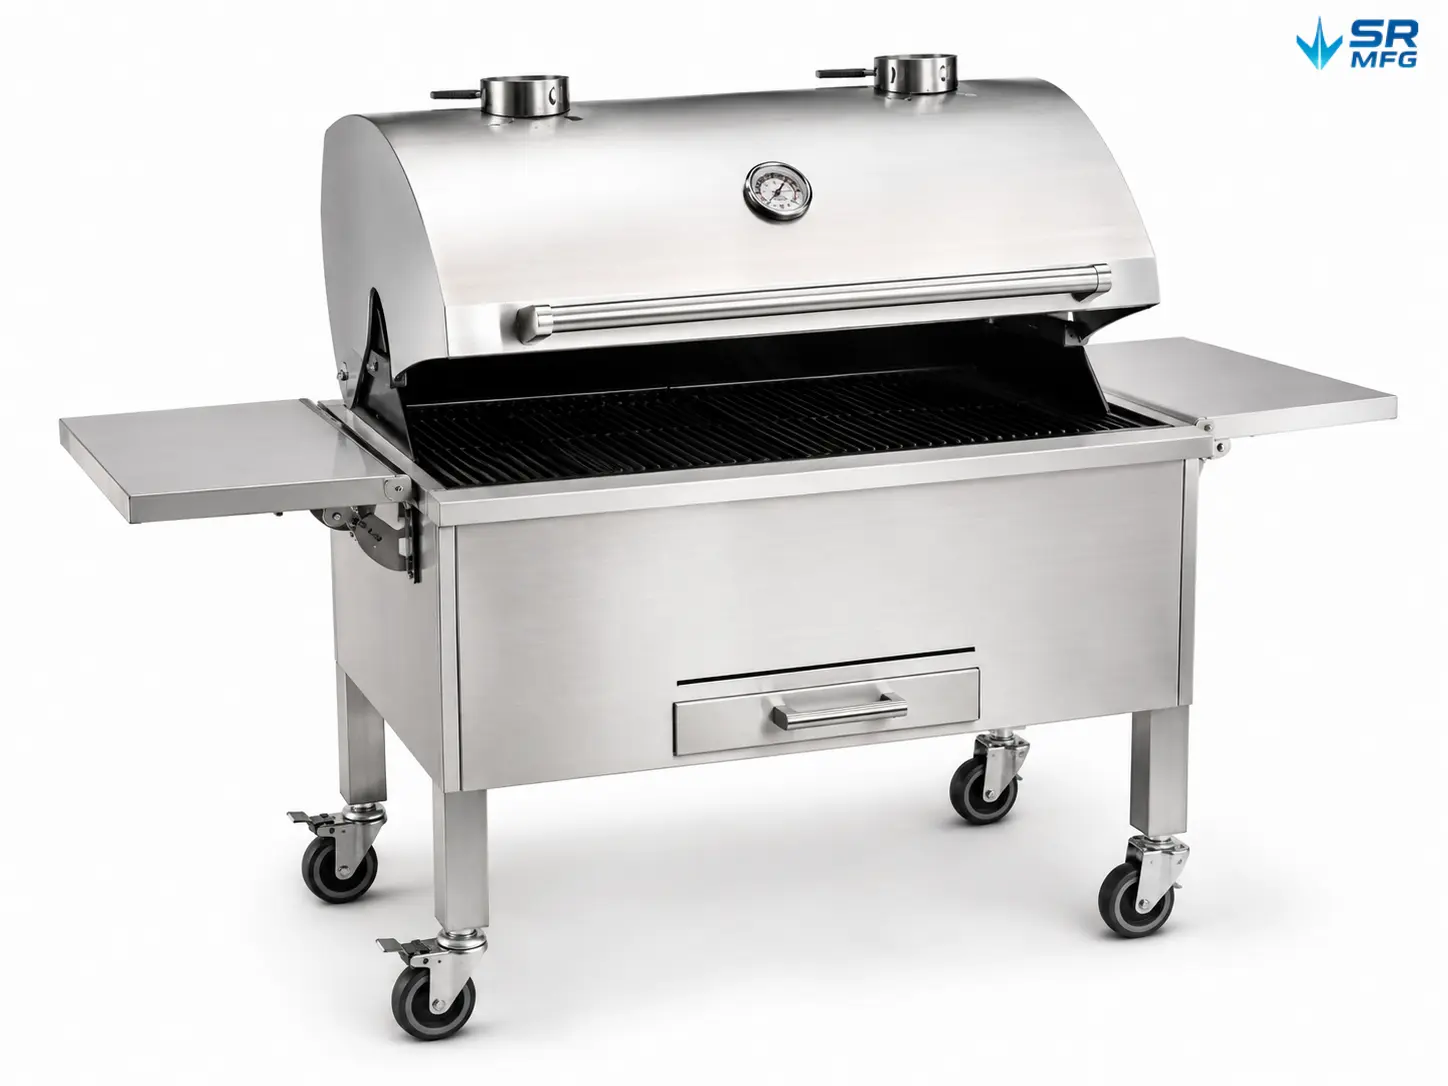
Weather-resistant spray painted finishes for outdoor enclosures, equipment covers, BBQ grills, lighting systems, and structural fixtures, engineered for UV stability, moisture protection, and years of fade-resistant color retention.
- 屋外設備筐体
- BBQグリル板金本体
- 保護カバー&パネル
- 取付ブラケット
- 耐候性構造部品
お客様の用途に合わせて設計
Whether you need a single sample or full production volumes, SR MFG ensures consistent coating thickness, uniform color matching, and reliable delivery for every spray painting project. We work with a wide range of paint systems including polyurethane, epoxy, acrylic, and enamel finishes to meet your exact specifications.
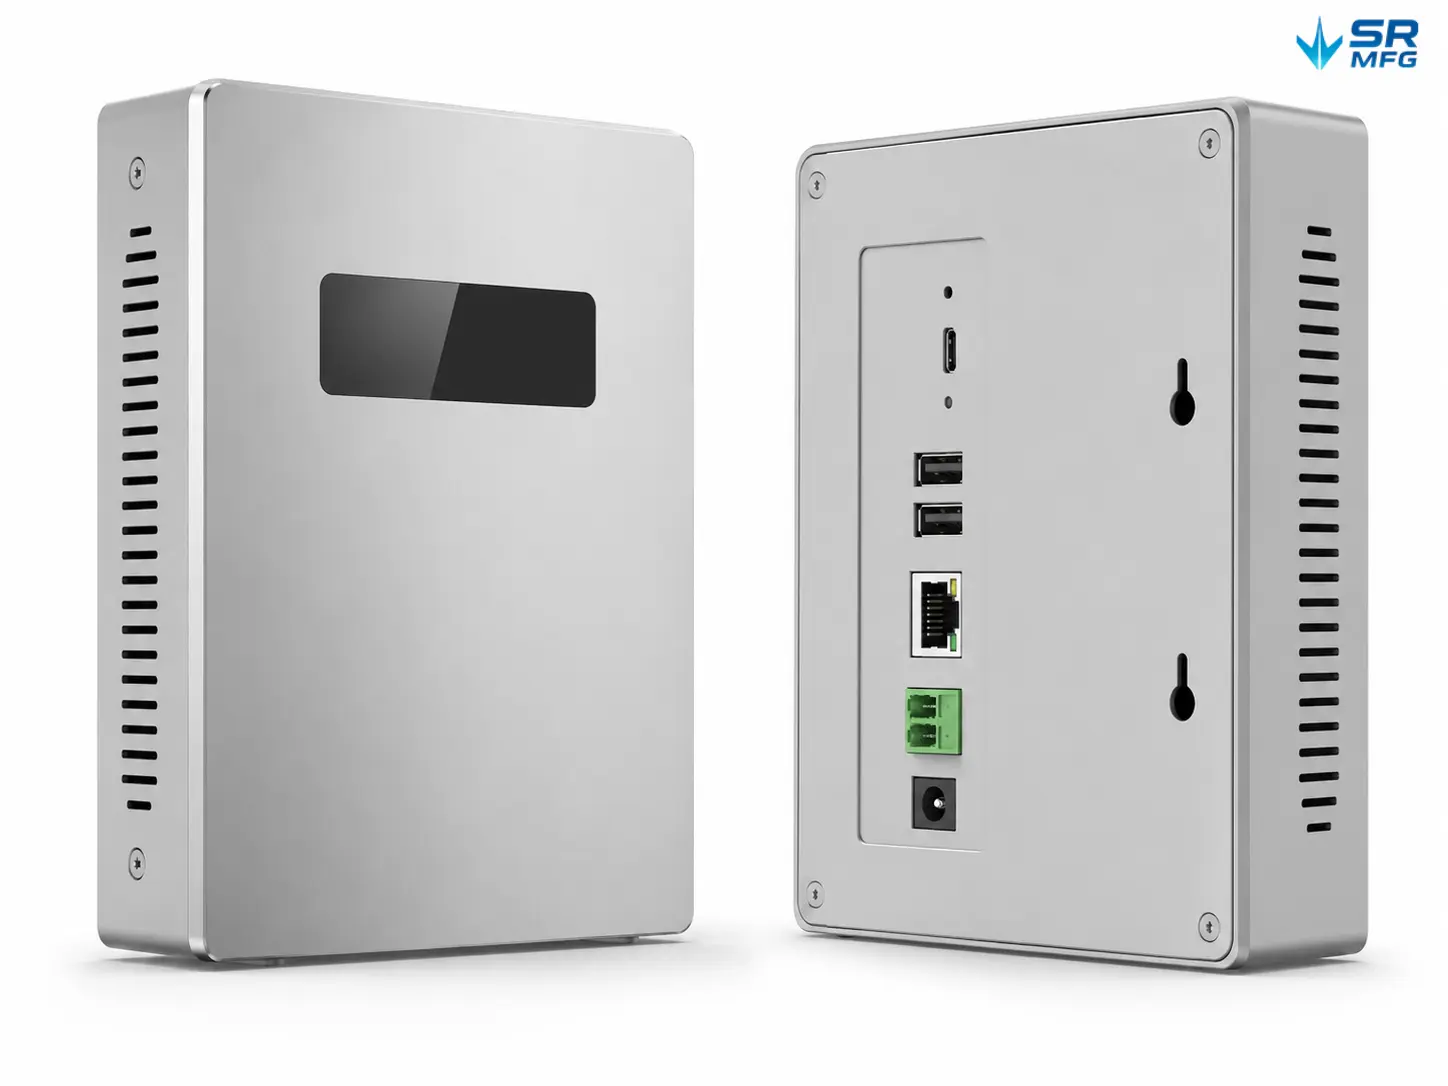
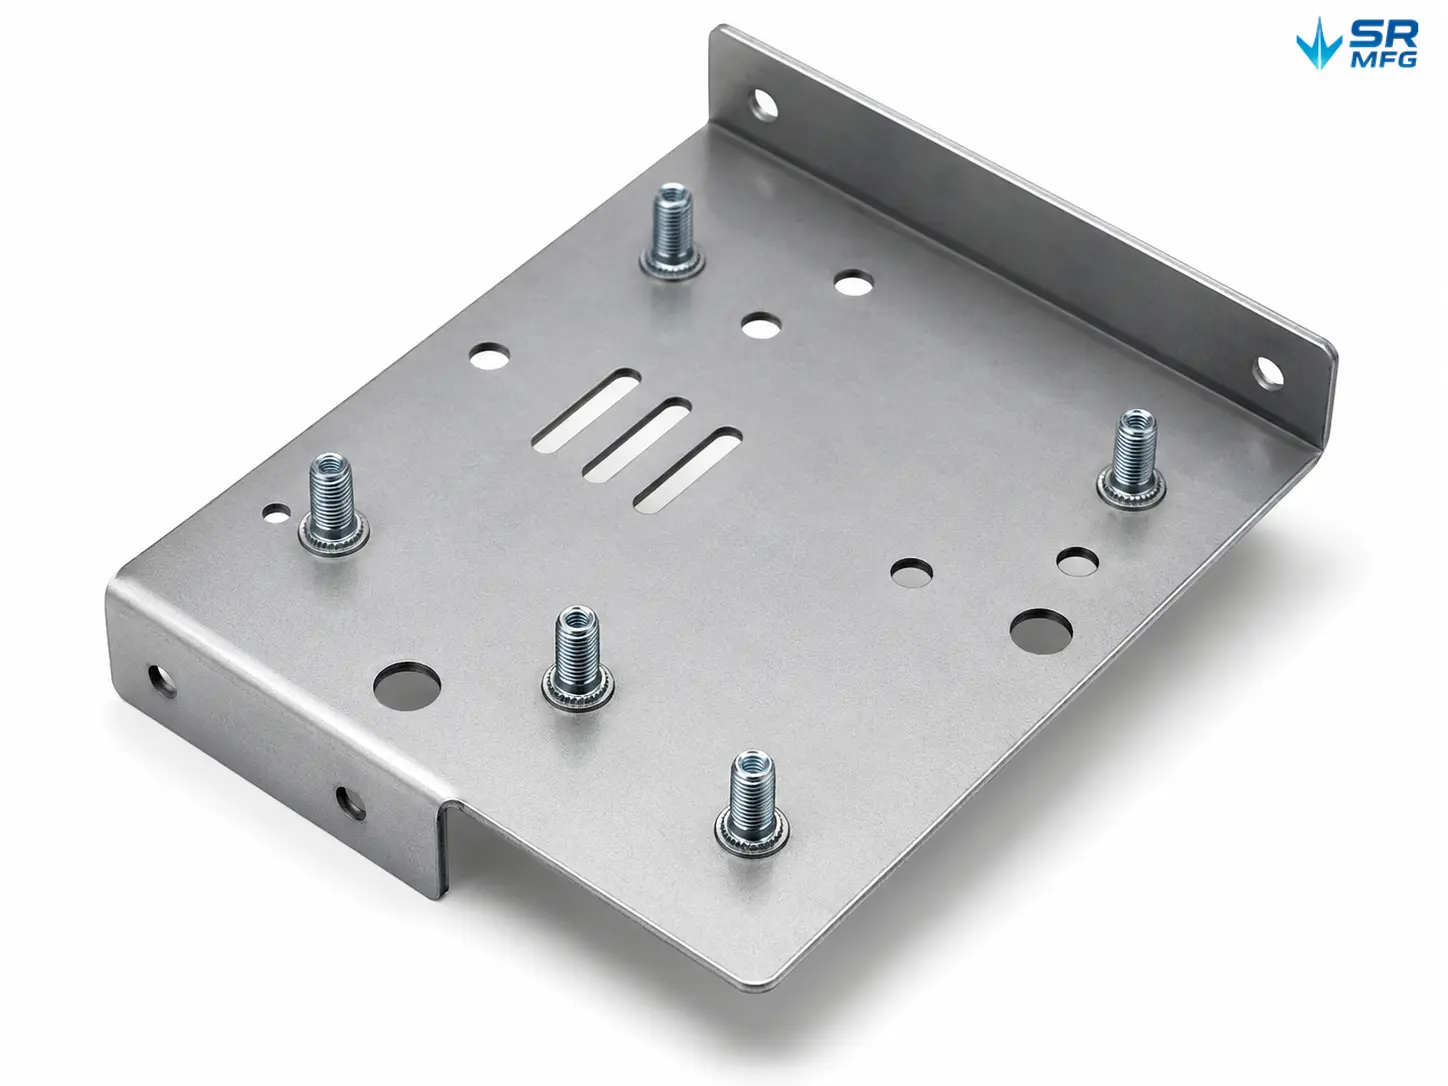
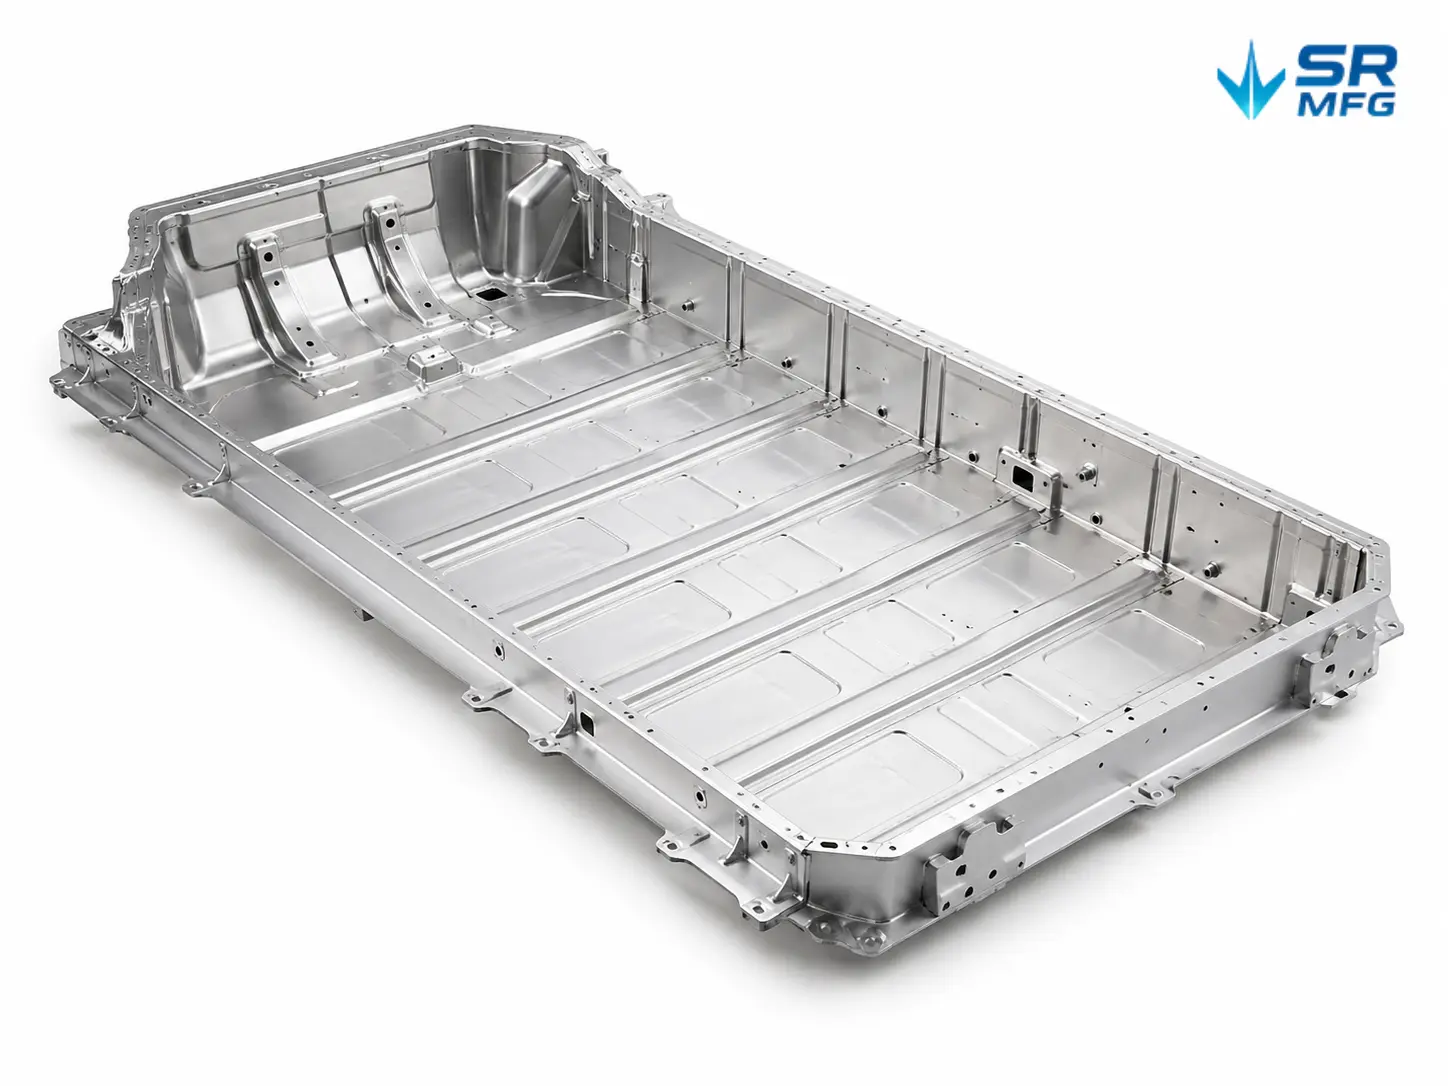
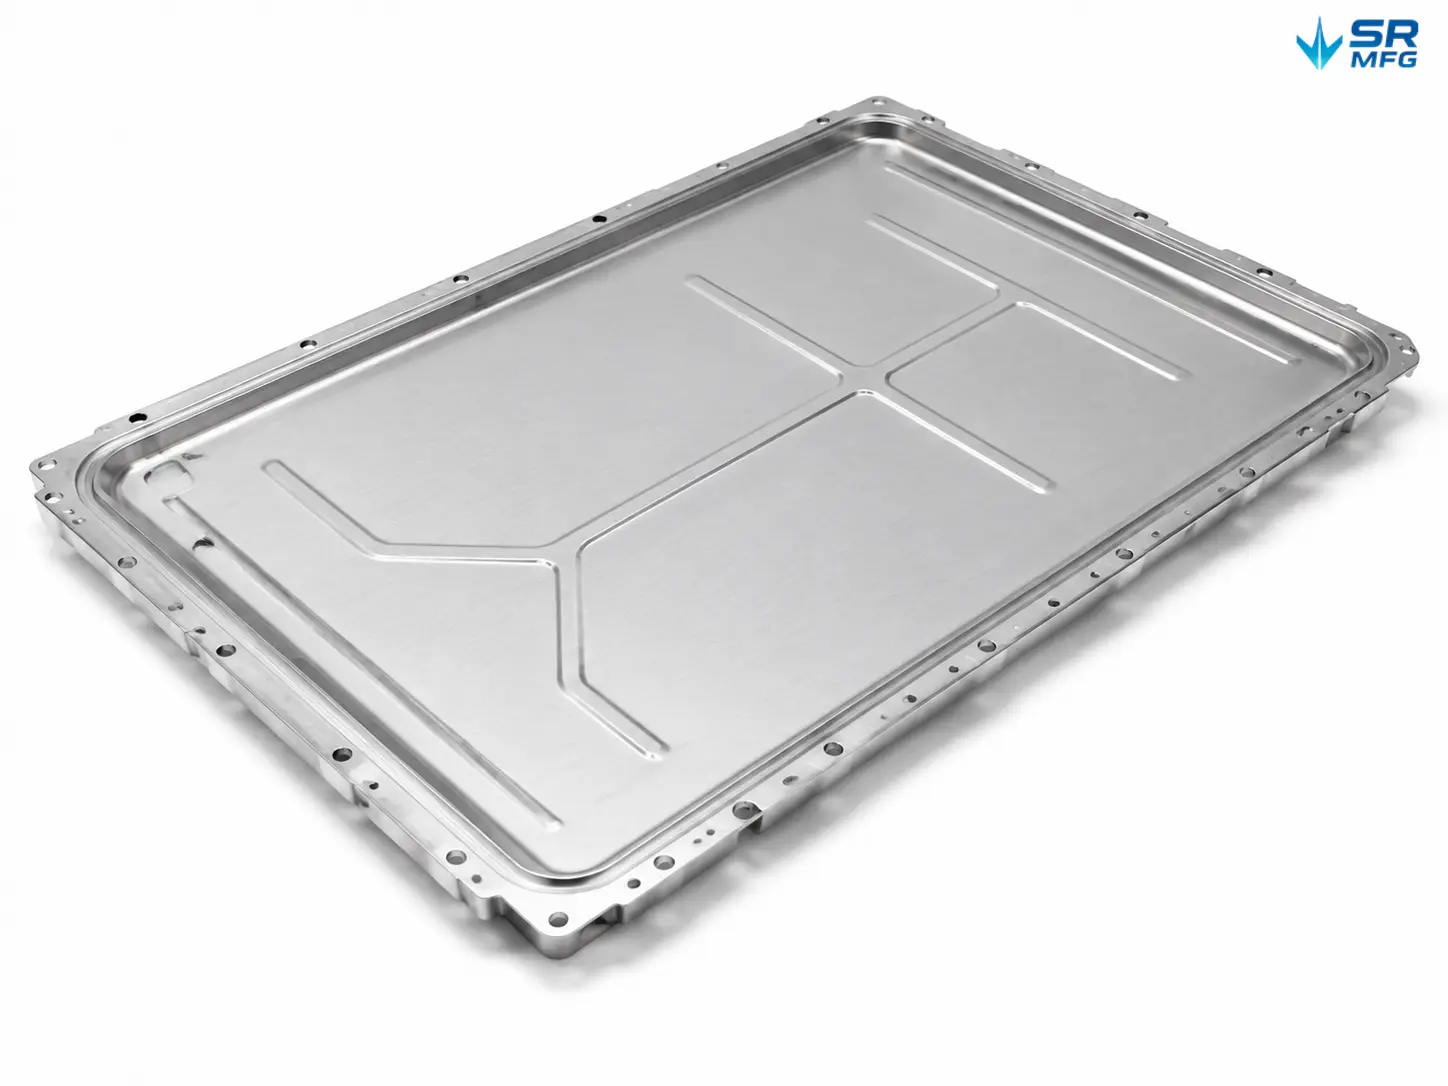
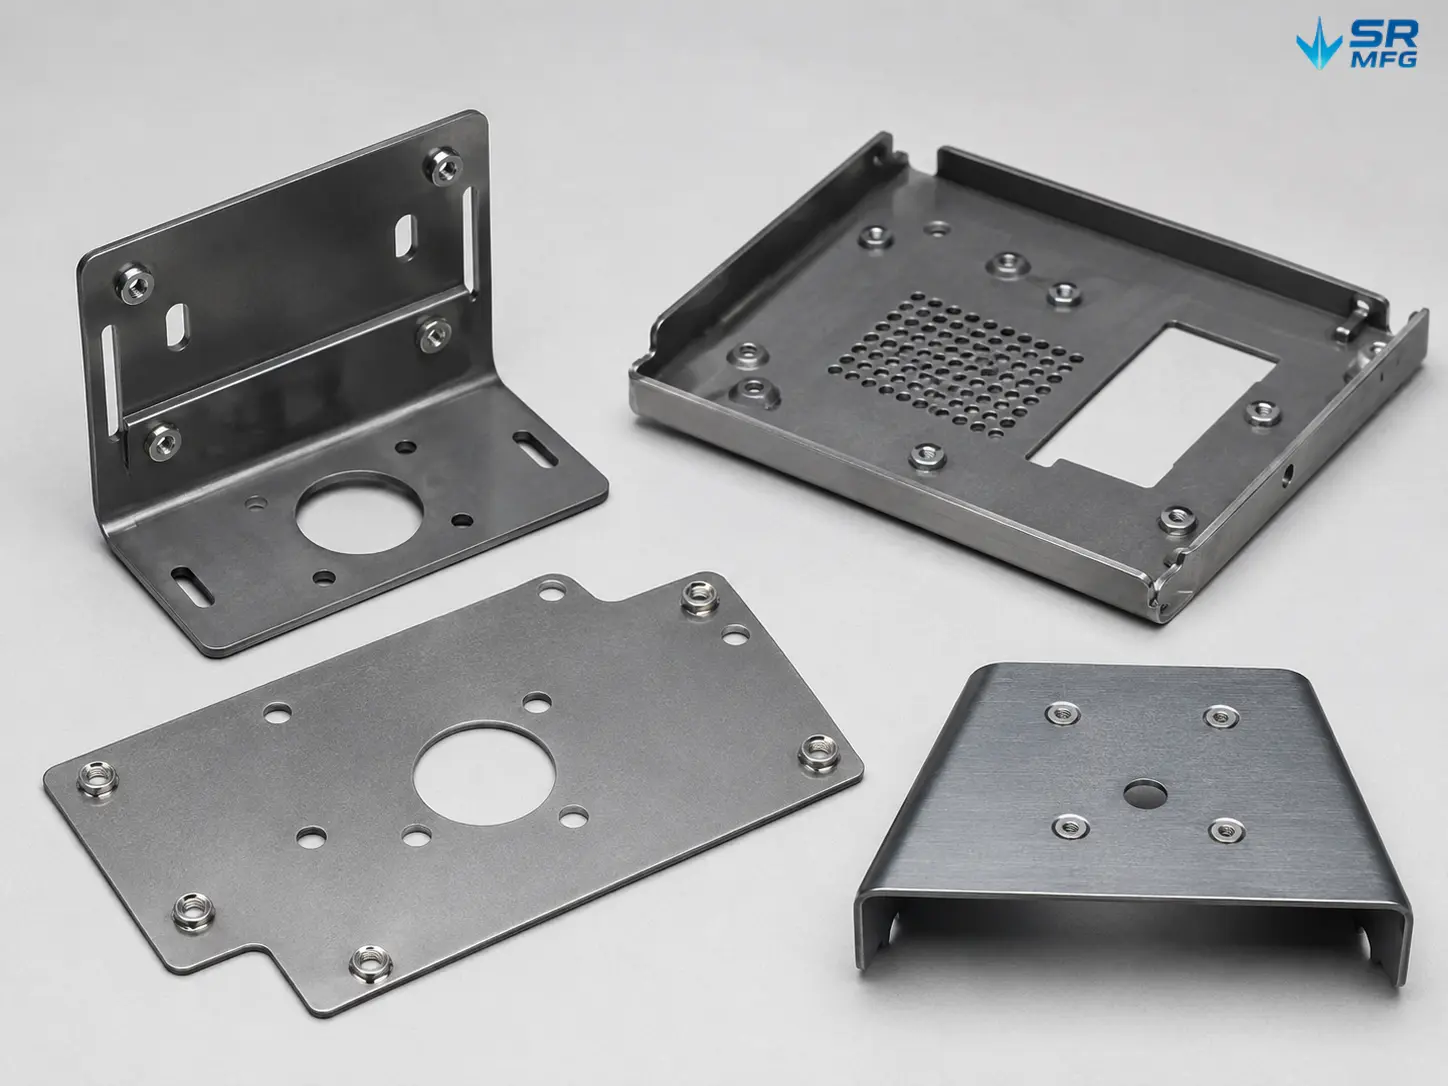
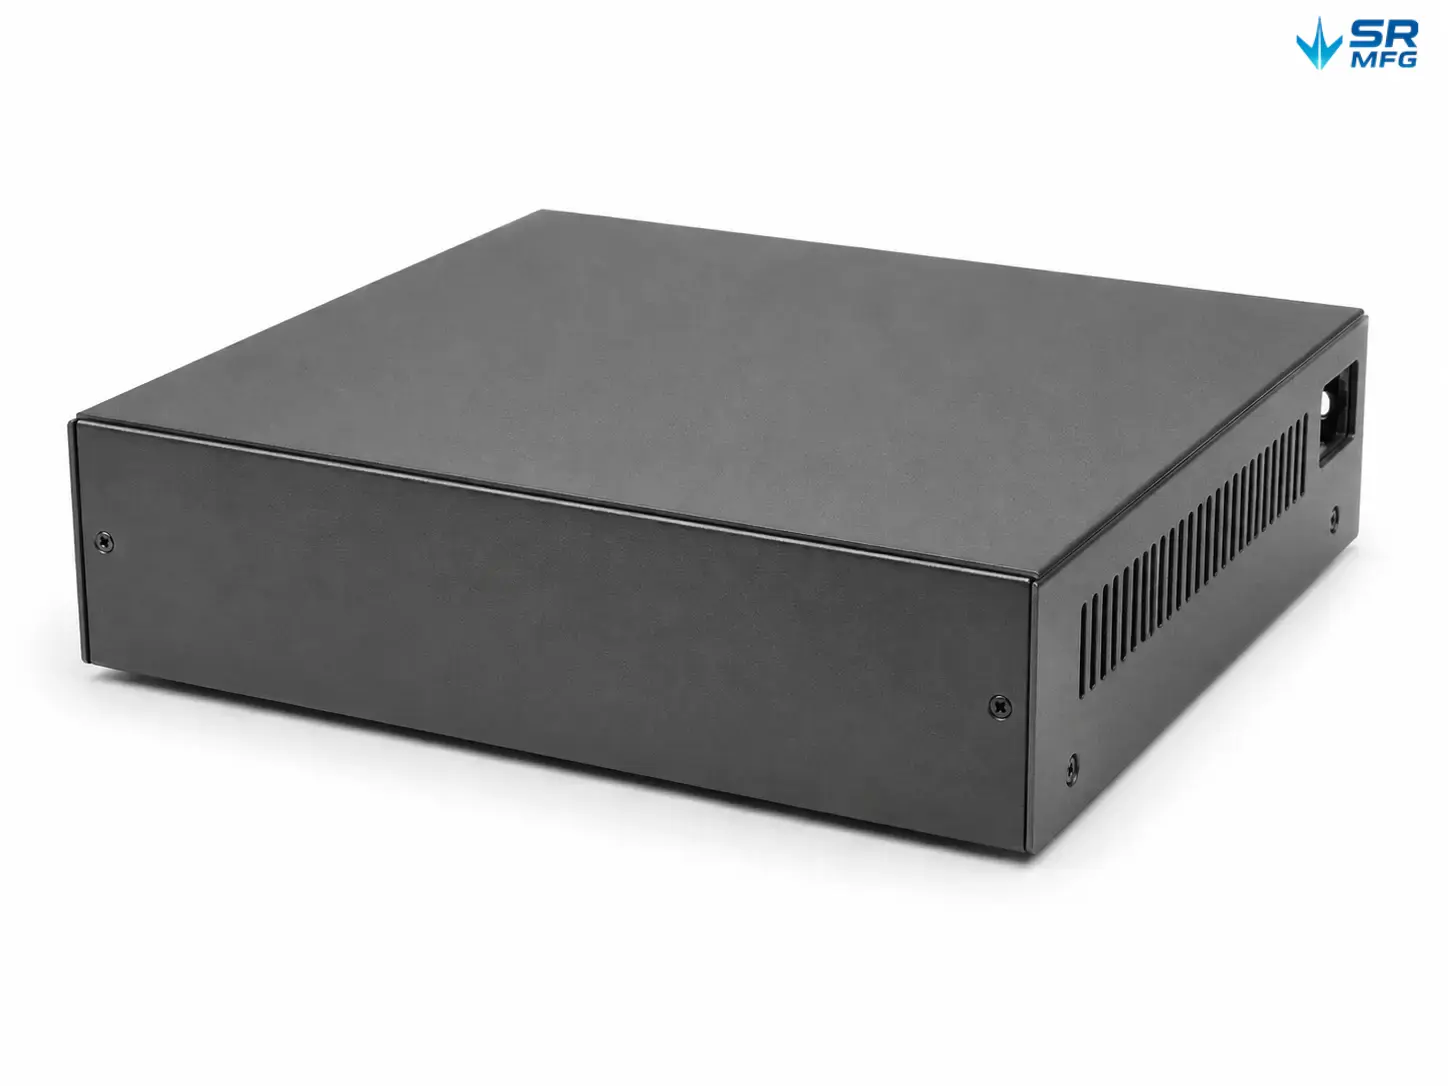
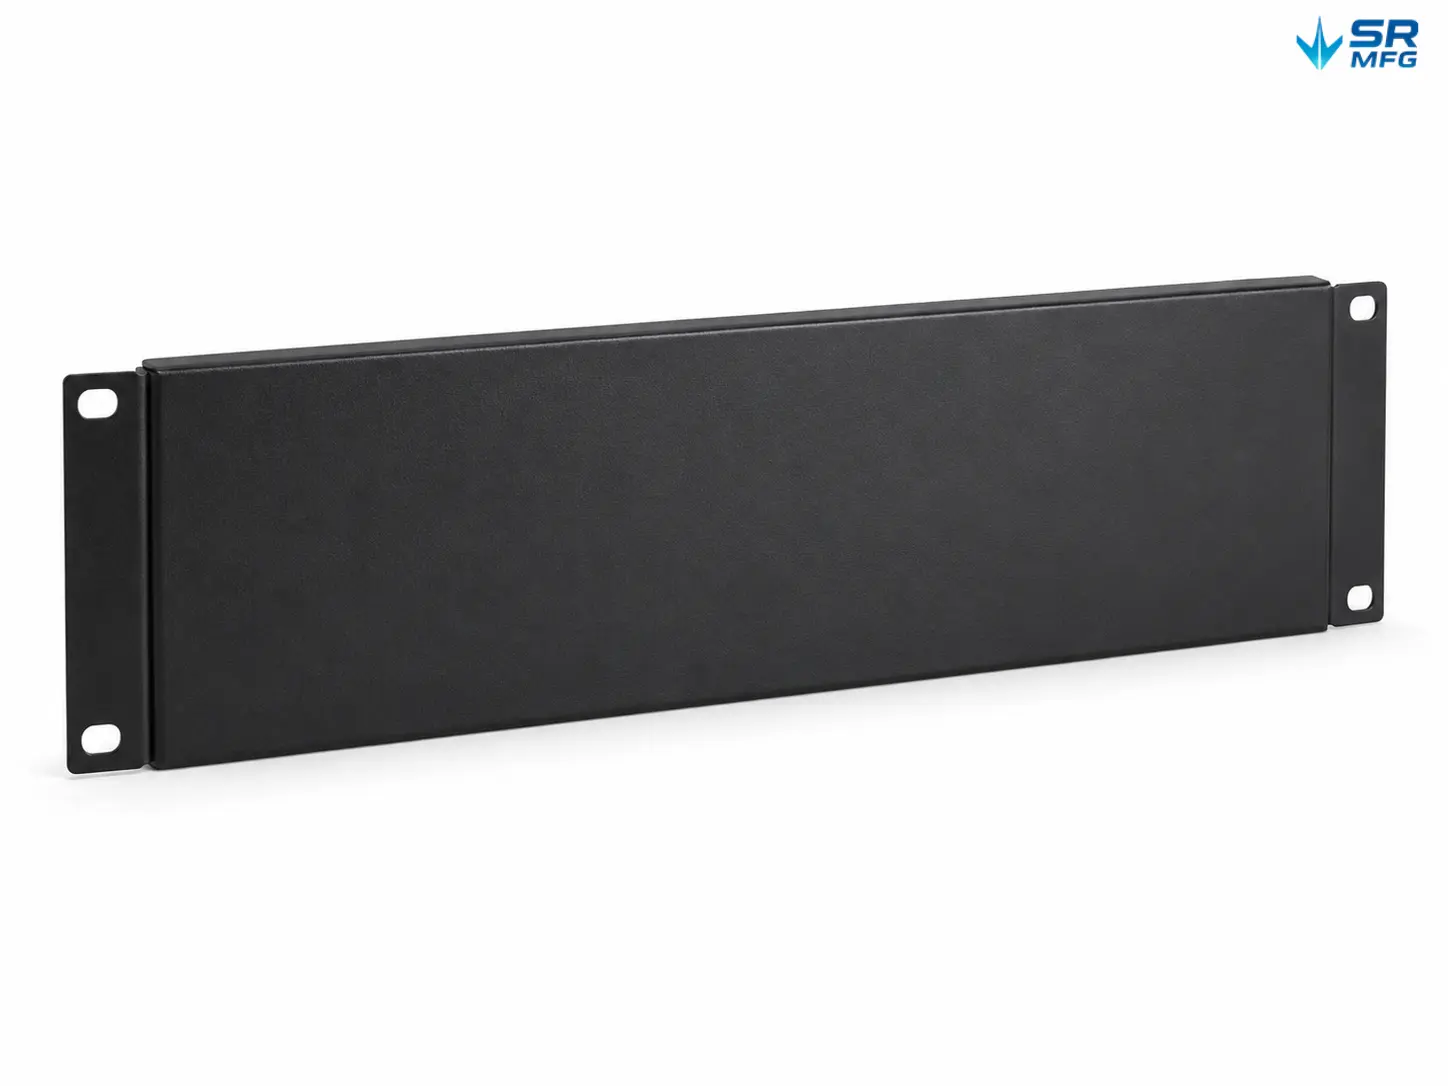
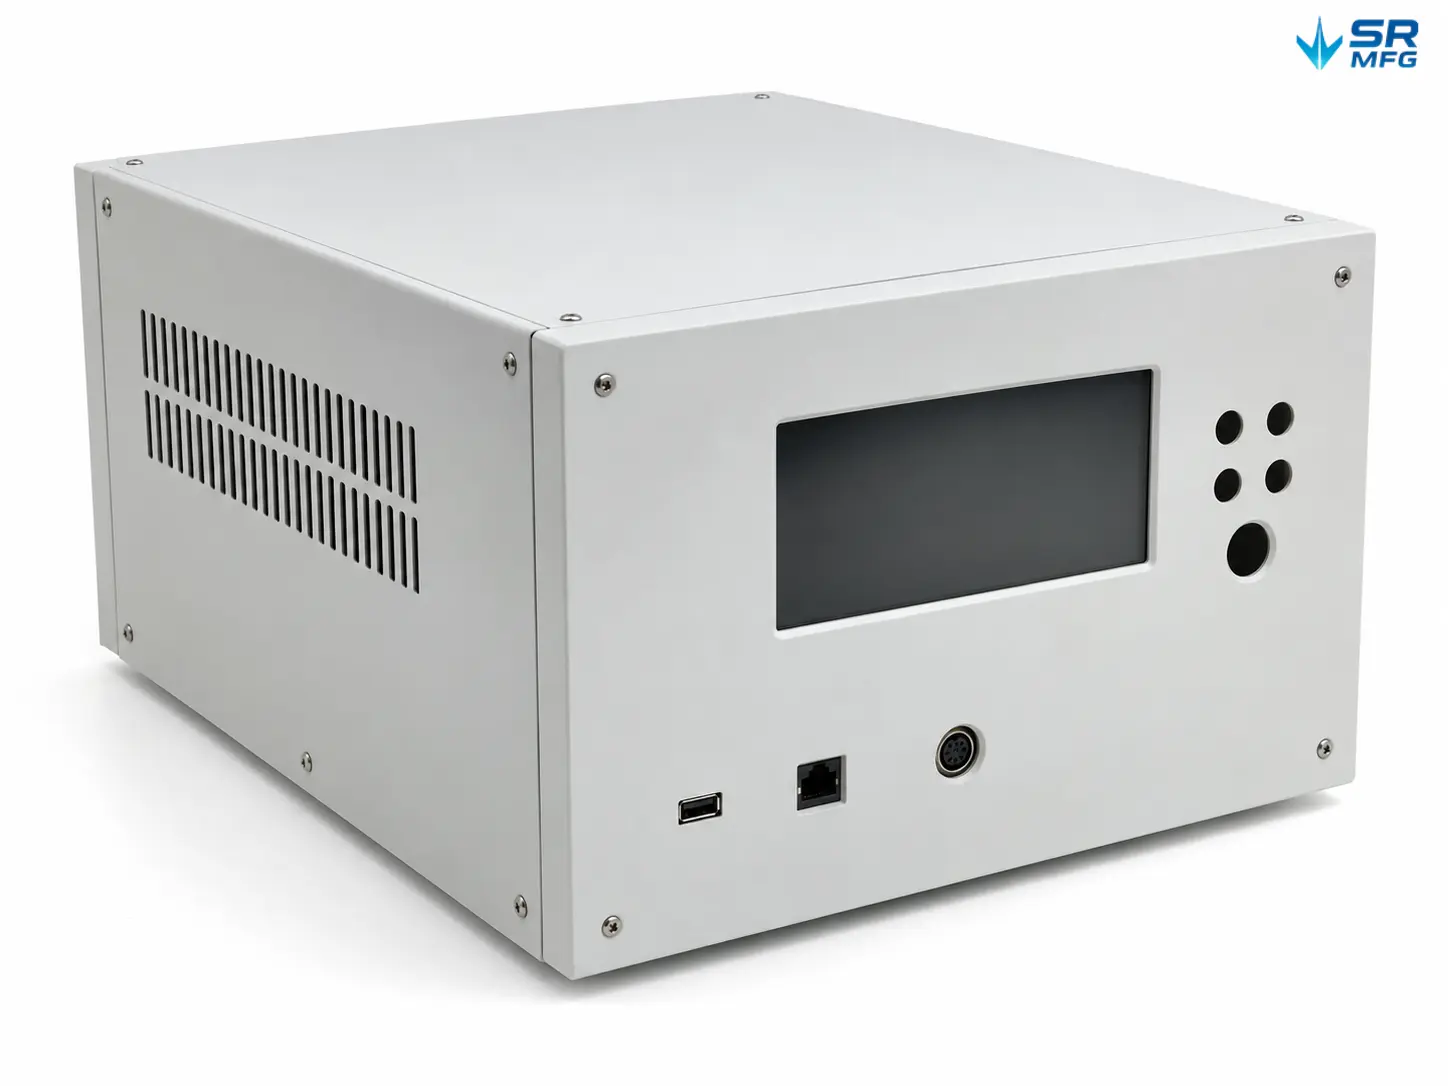
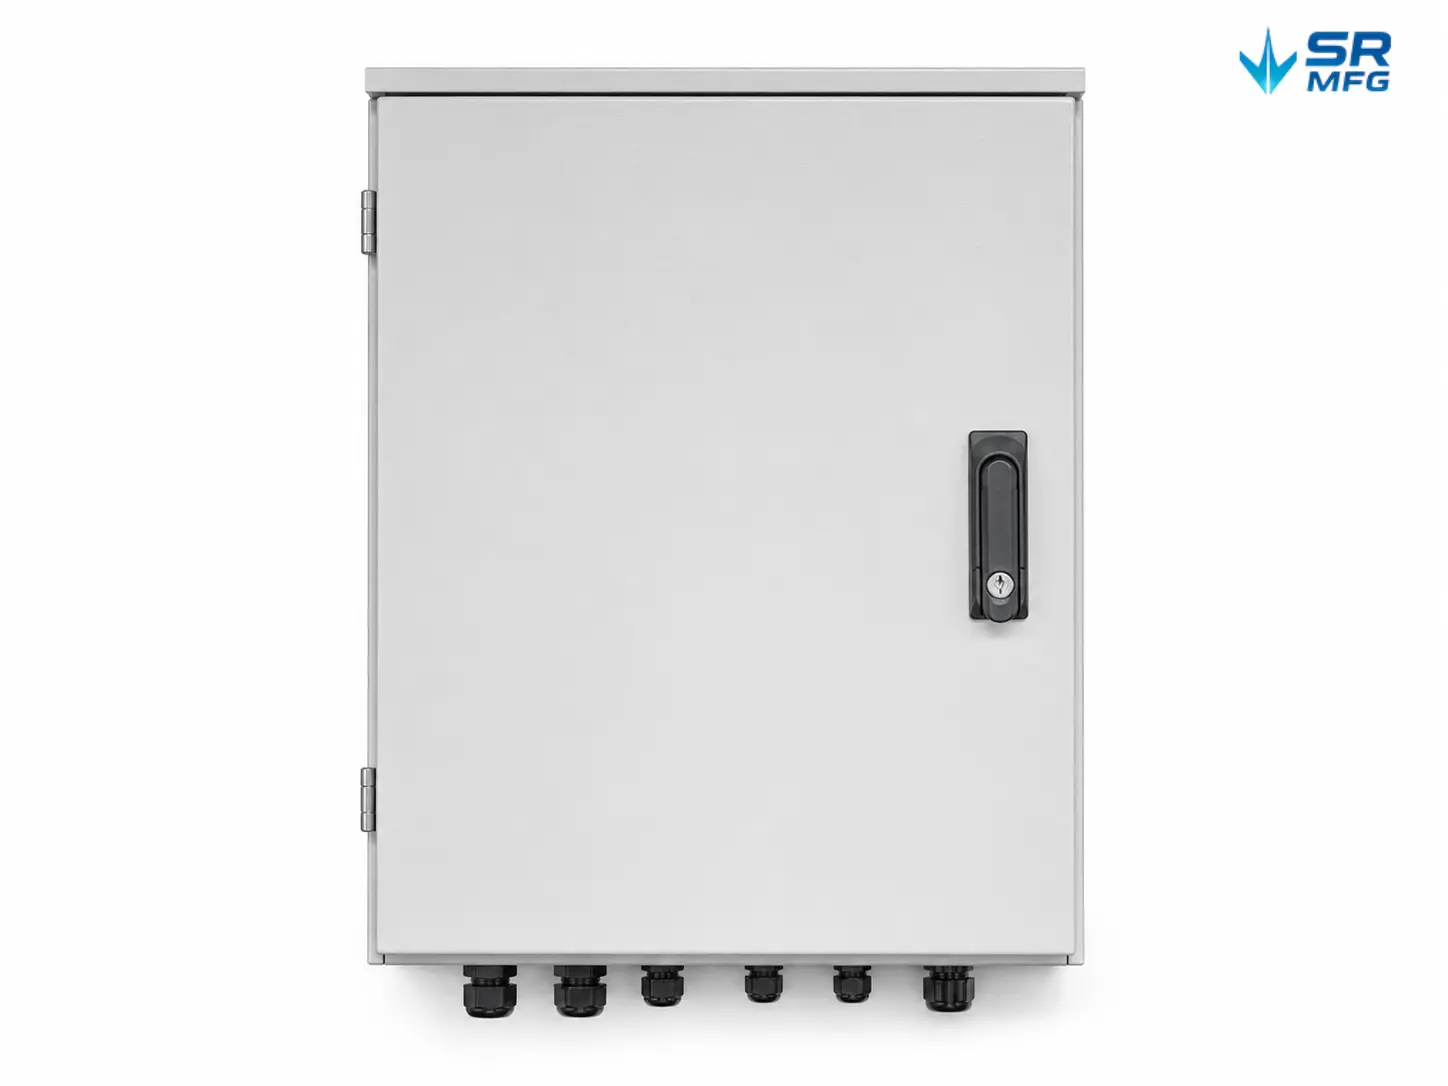
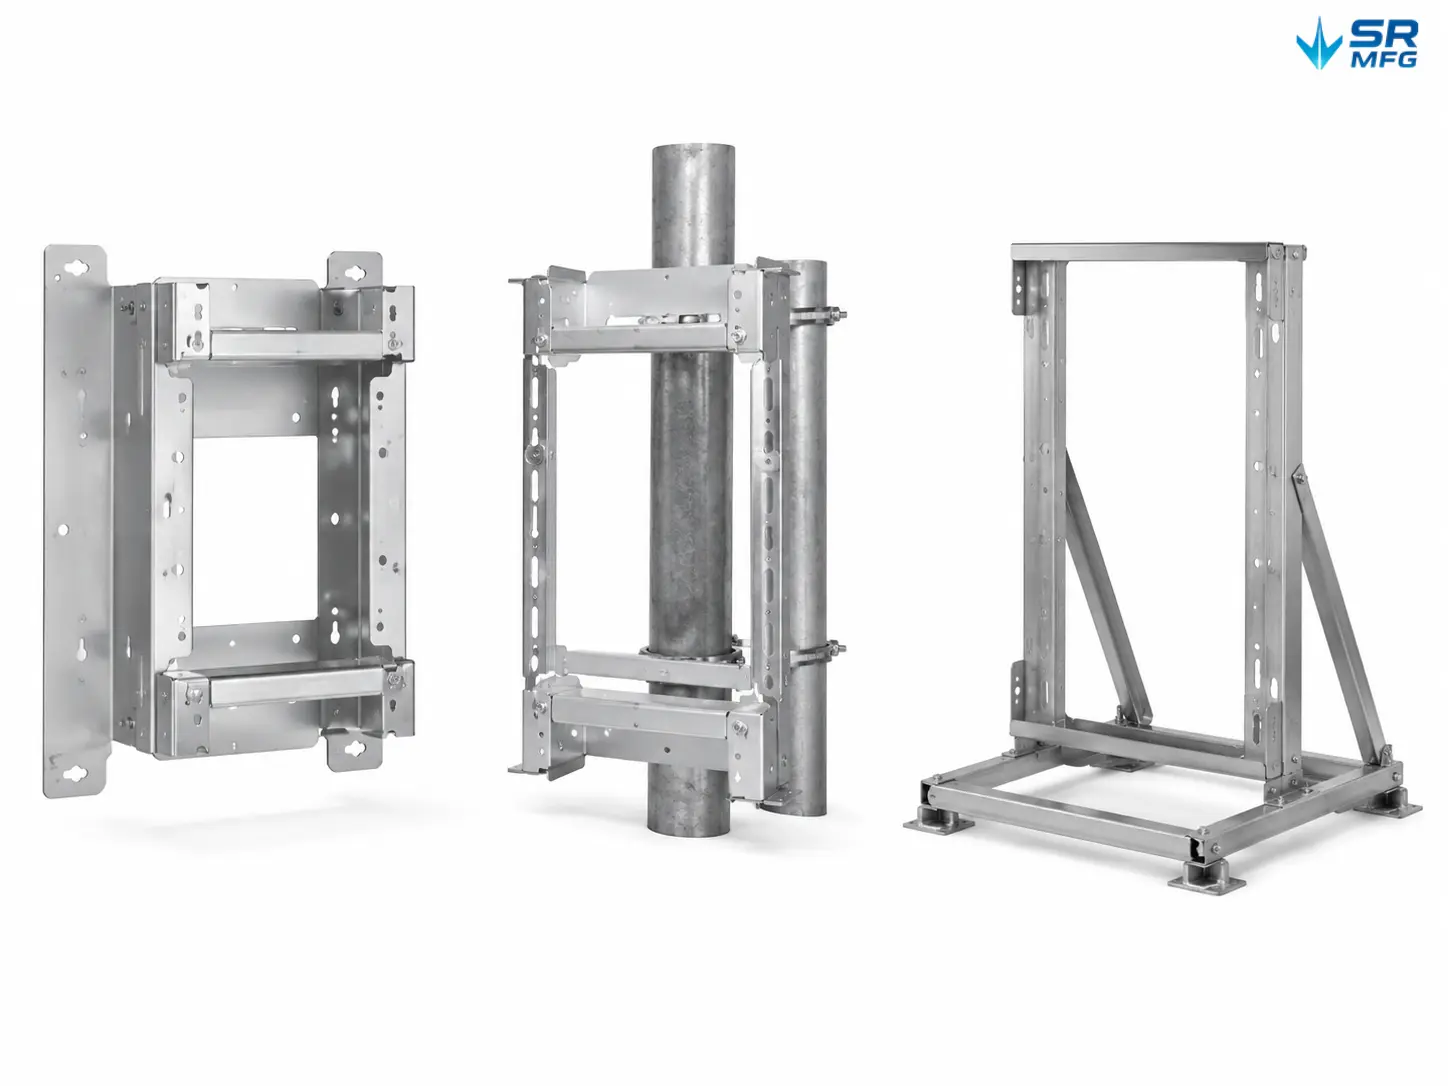
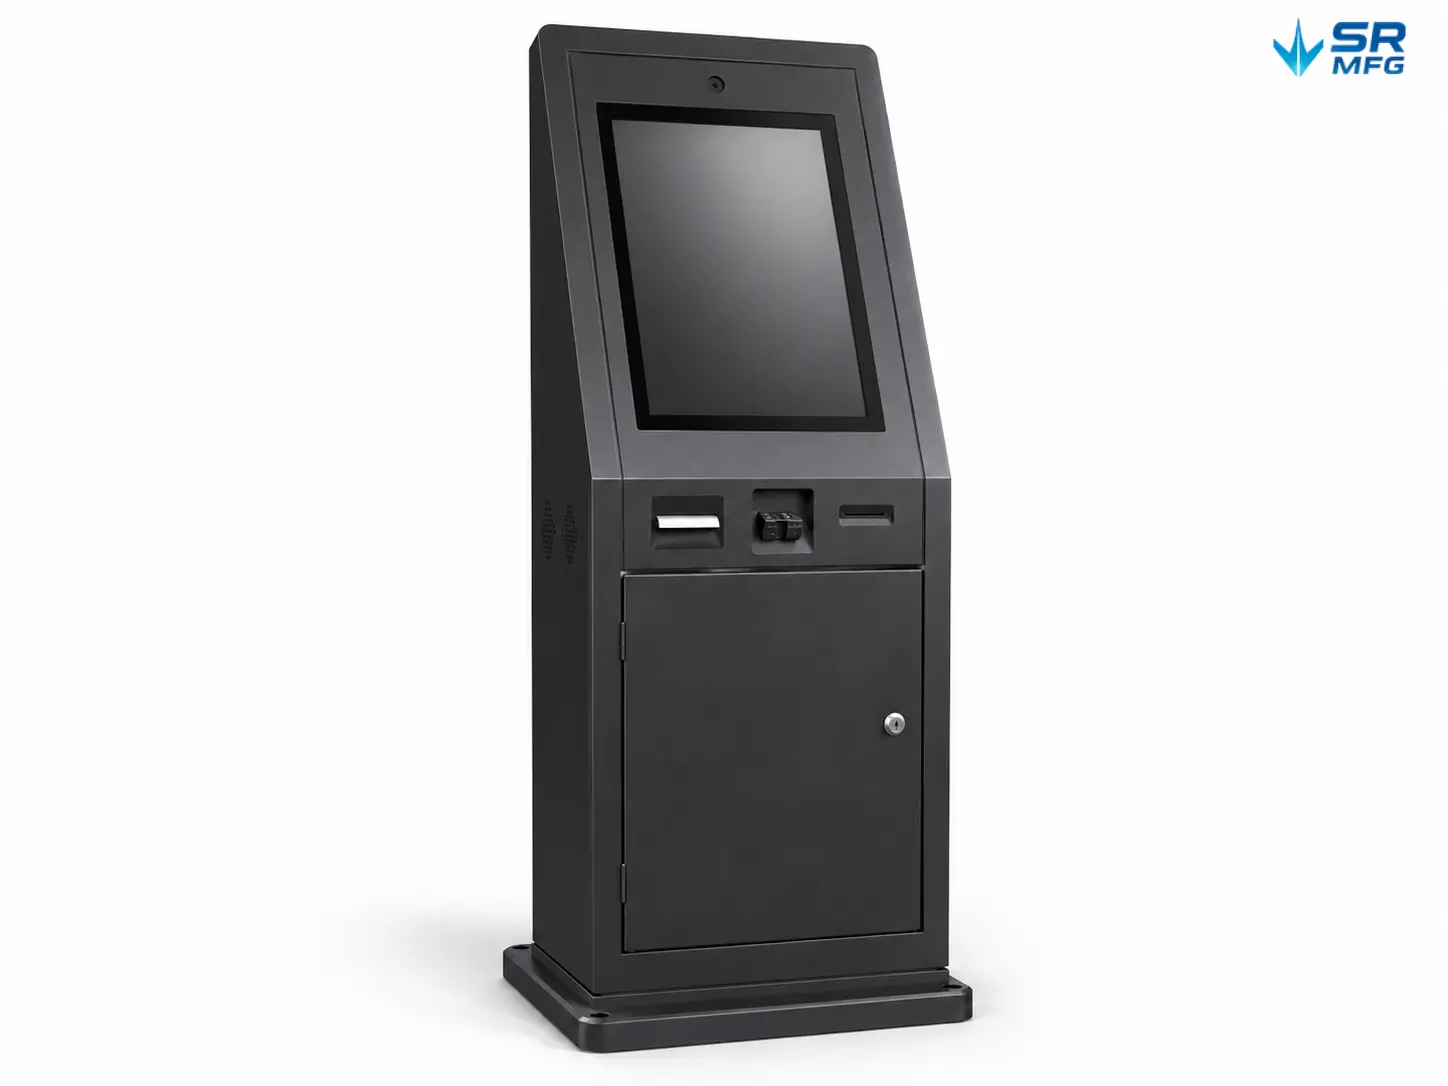
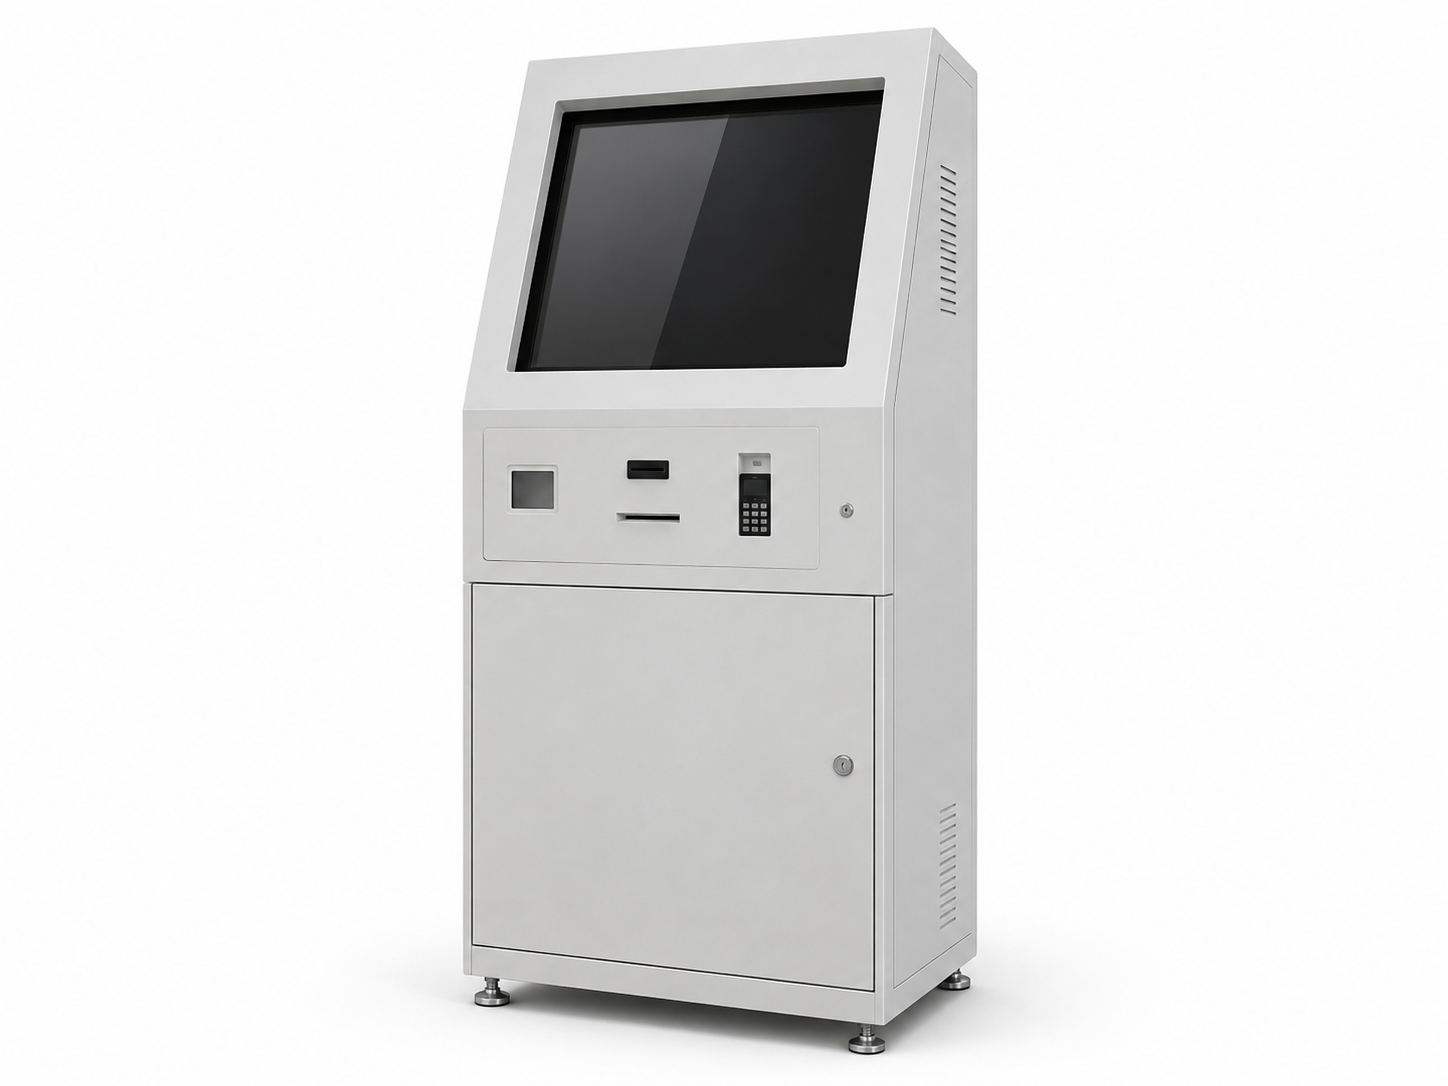
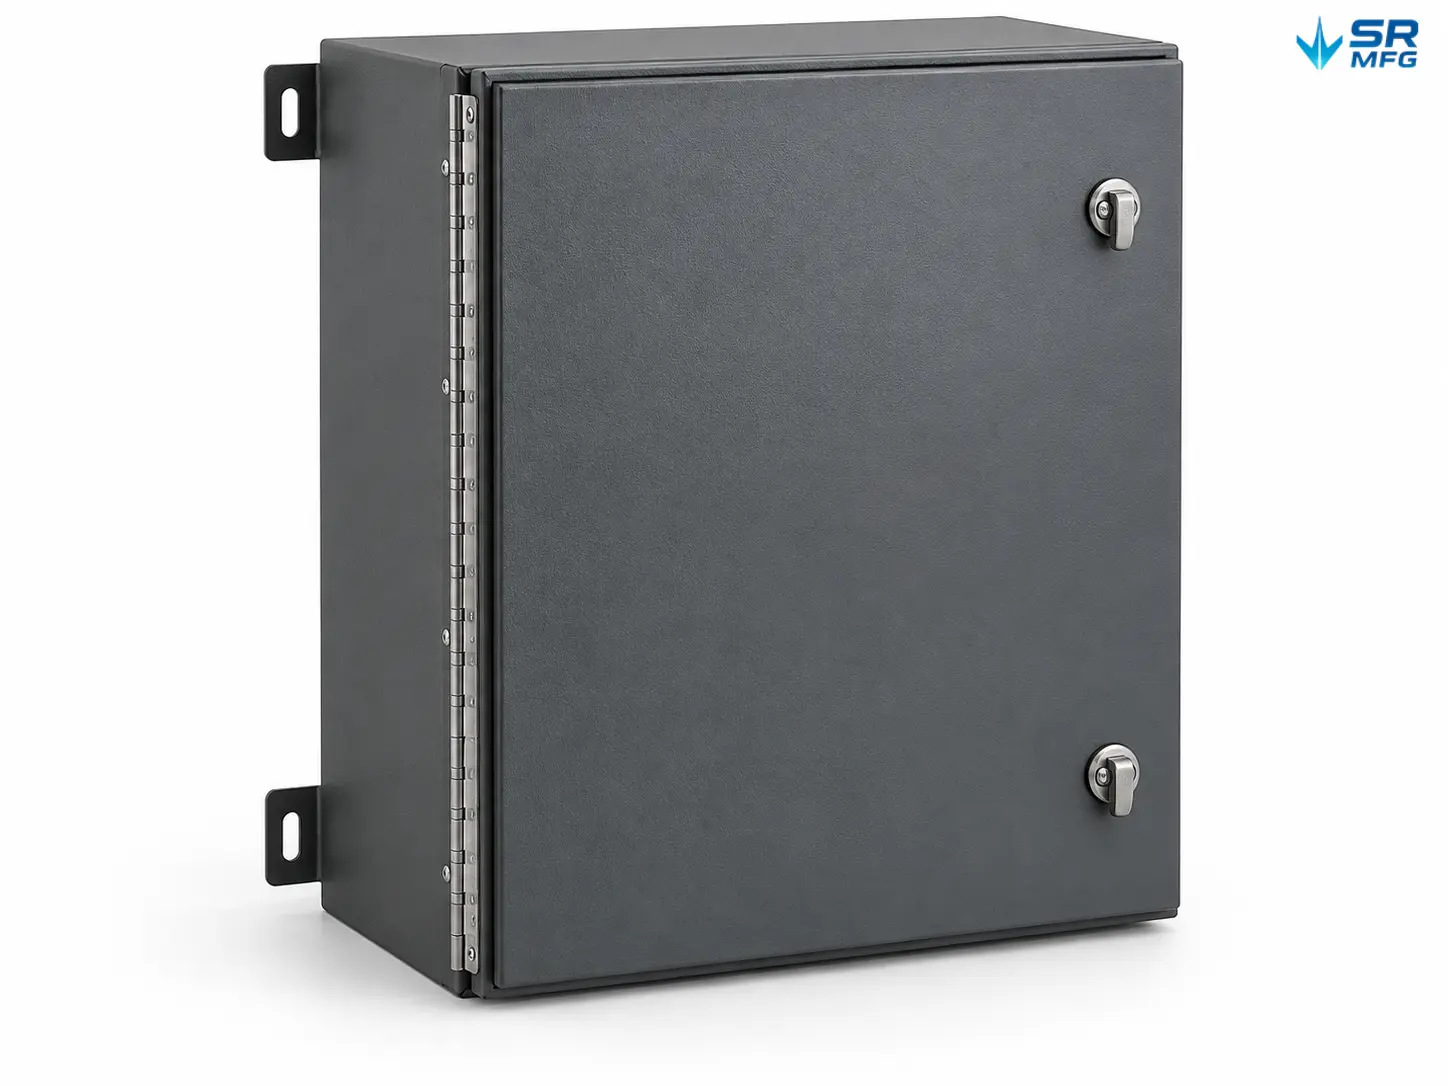
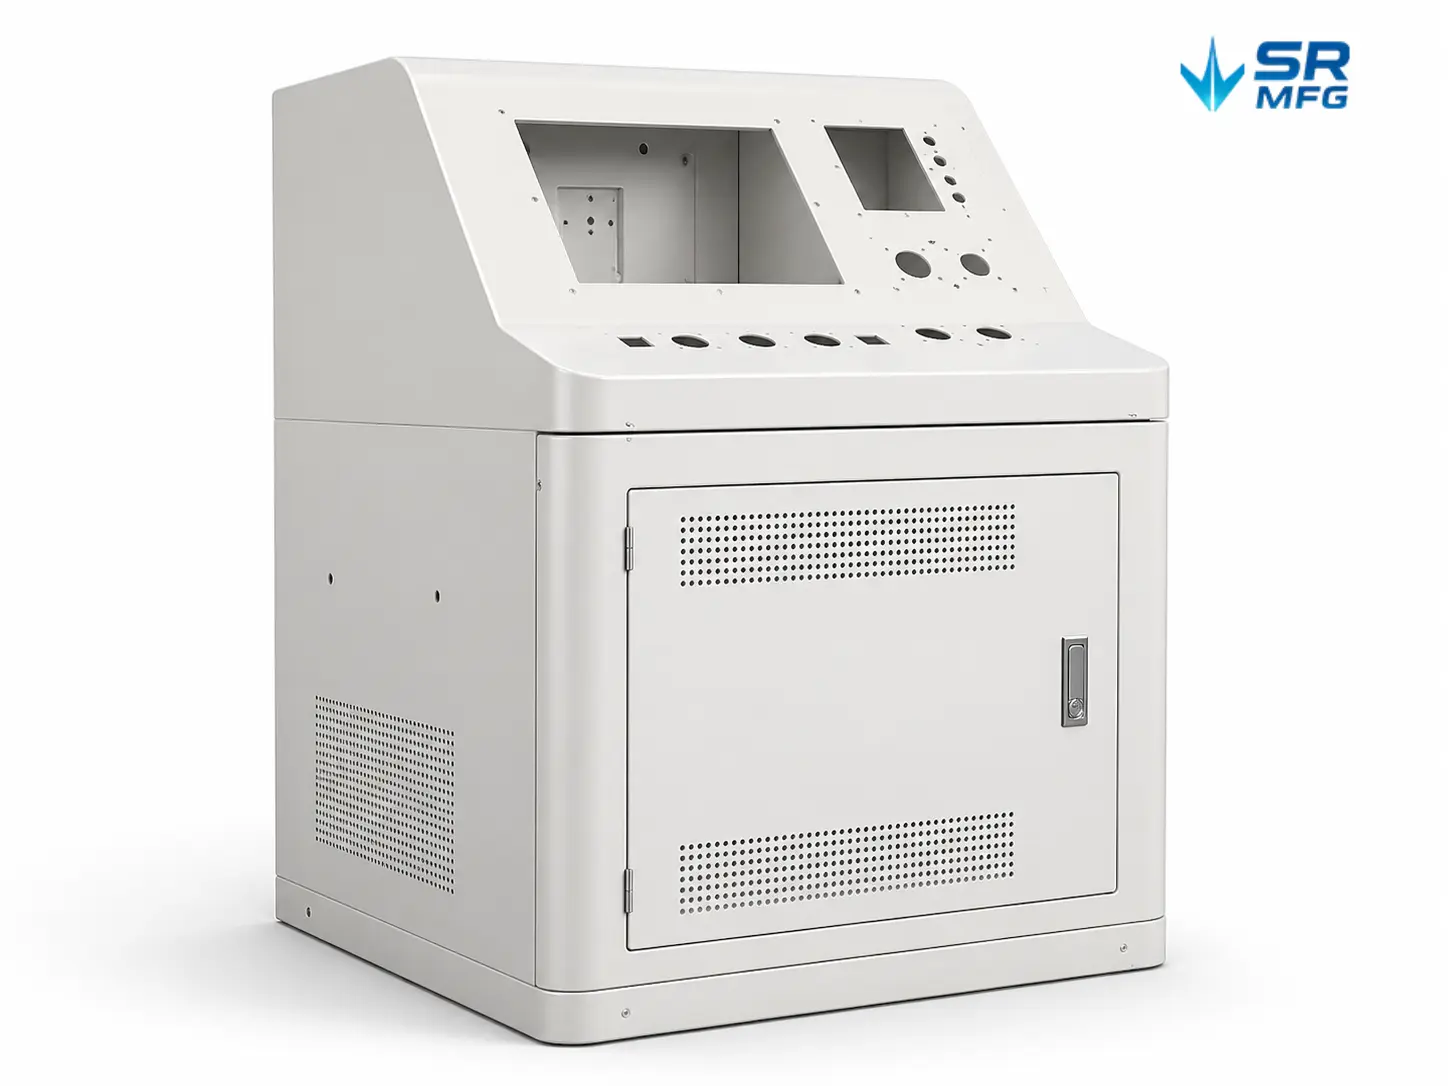
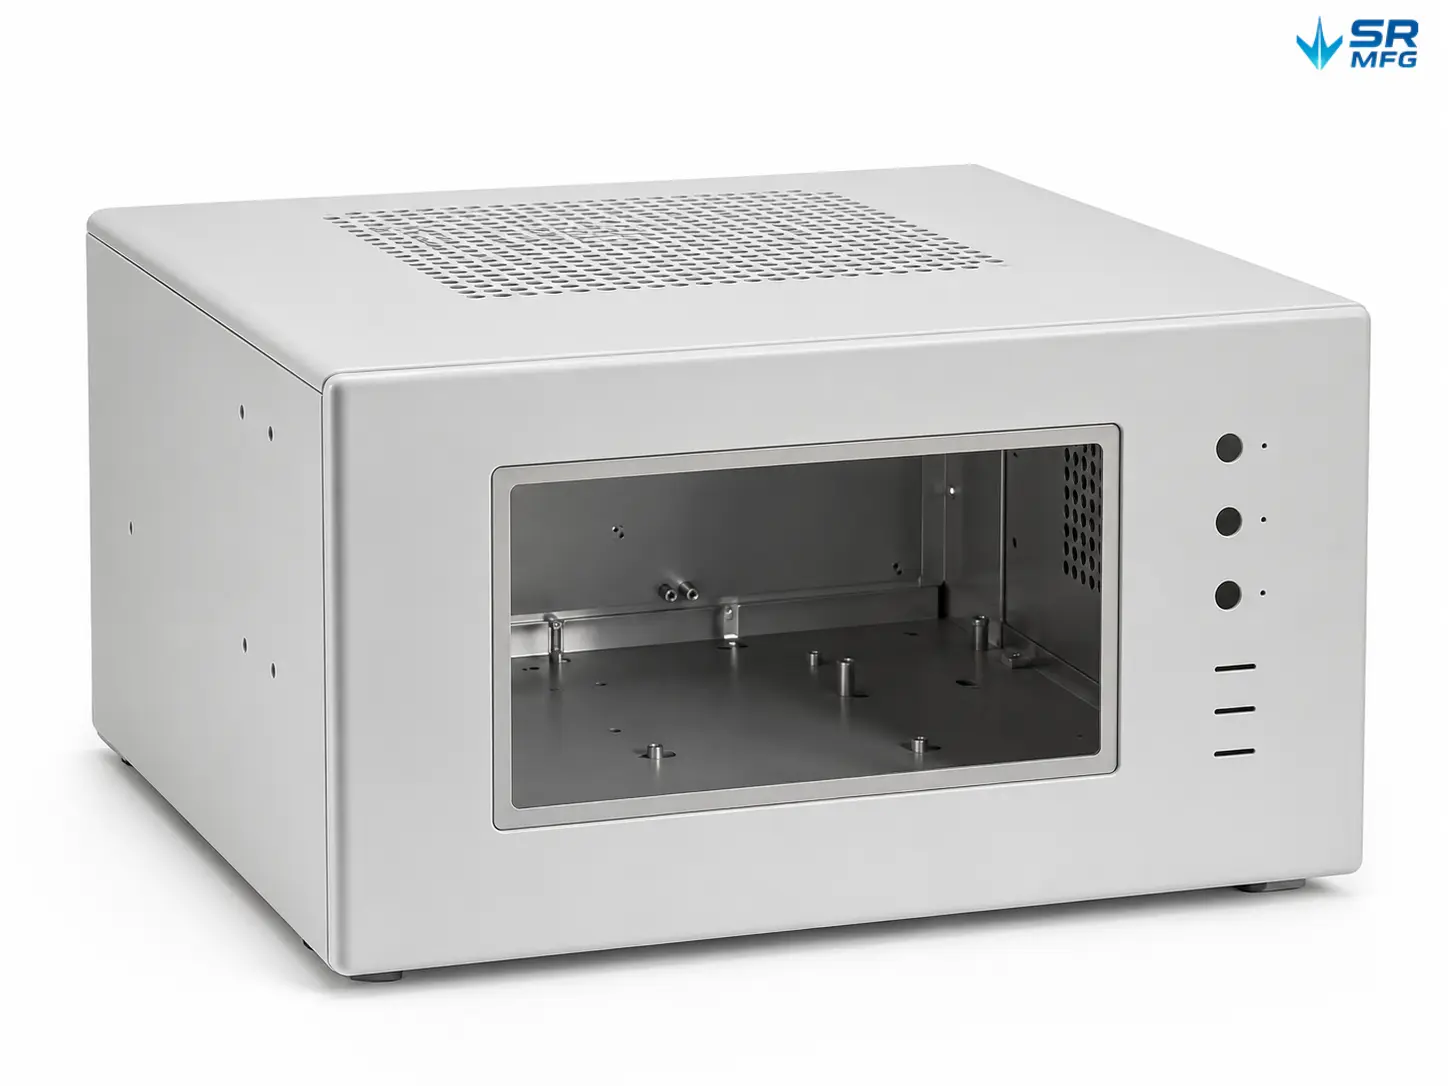
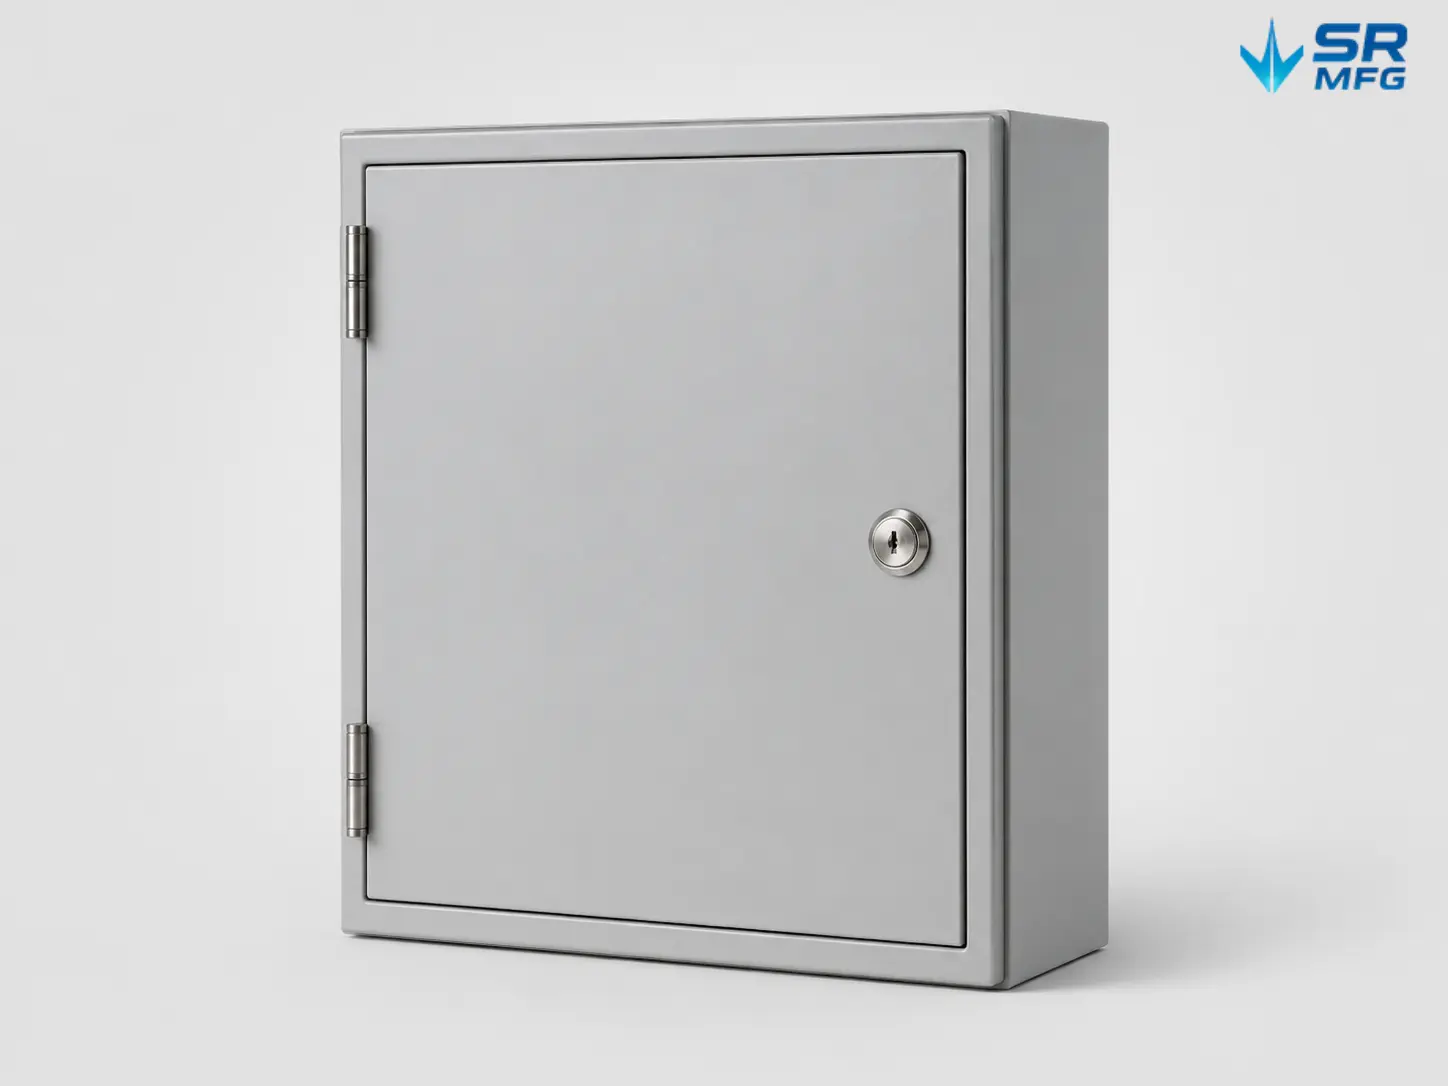
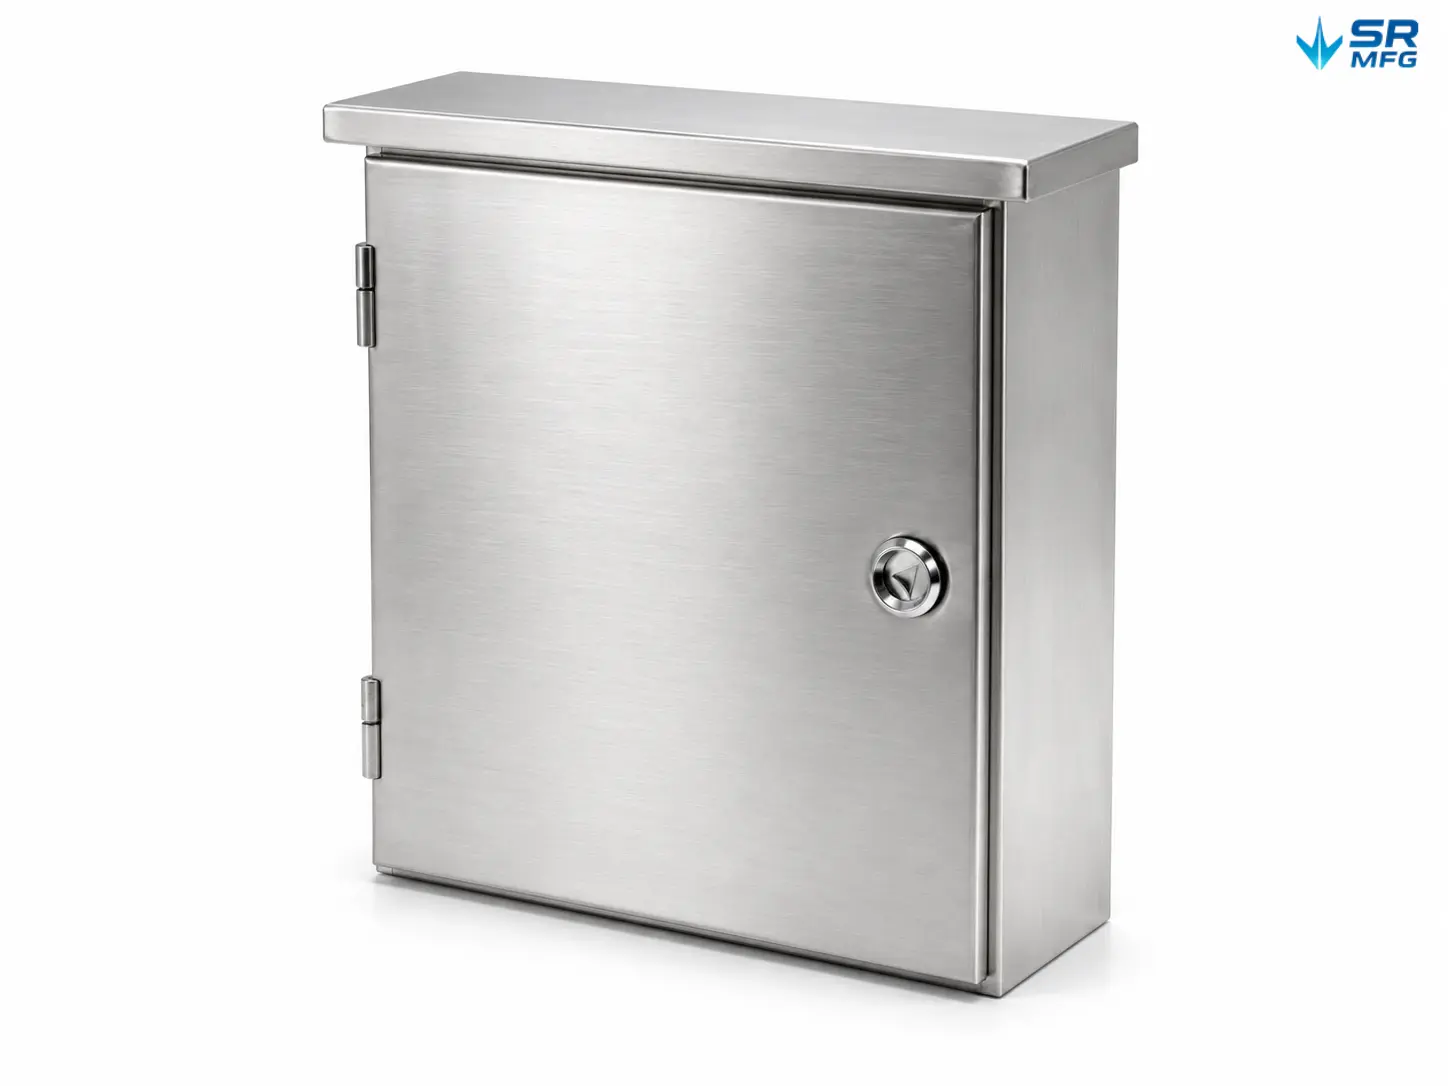
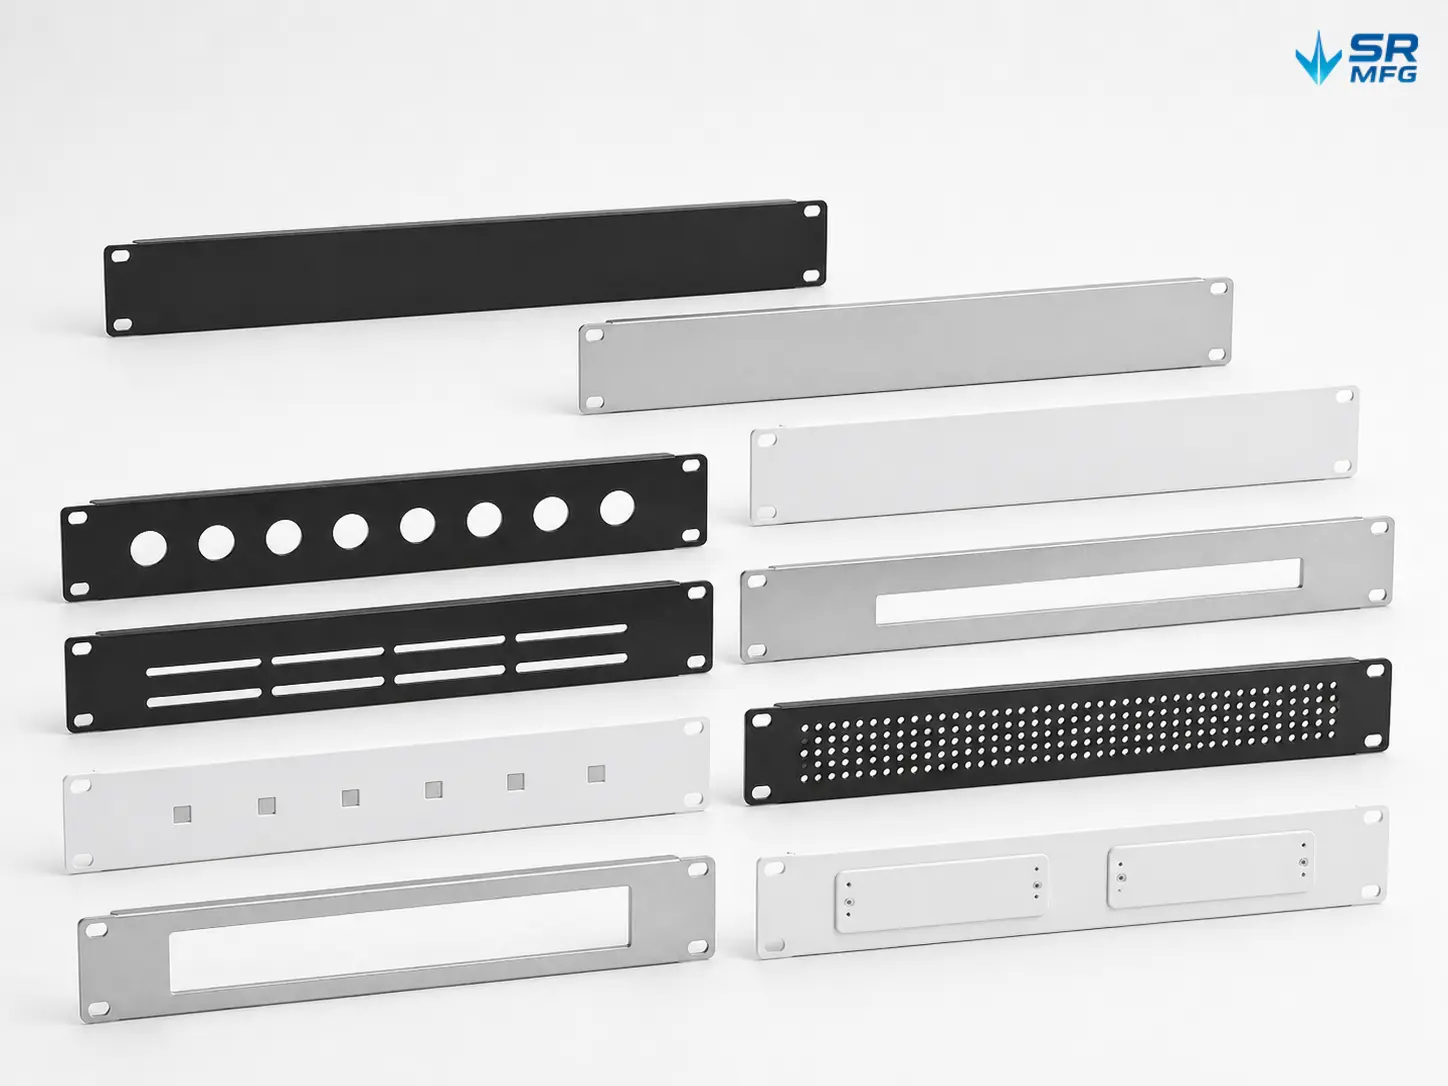
SR MFG Metal Spray Painting Product Showcase
Sheet Metal Spray Painting よくある質問
Coating thickness is set based on your desired appearance および corrosion protection requirements. If needed, we can recommend a target thickness range and measurement locations during quoting.
When certain areas require tight thickness control or must remain uncoated, we typically use a combination of:
-
Masking for thickness control: High-temperature tape, masking film, or plugs to protect no-coat zones or limit build on critical areas.
-
DFM design recommendations: Adding small steps/ledges or masking features so masking lines don’t land on visible cosmetic surfaces.
-
Inspection and records: DFT is measured at agreed locations and recorded using ASTM D7091 (or an equivalent standard).
SR MFG matches color to RAL/Pantone standards or your supplied sample. We follow a defined process to ensure consistency: sample approval first, then we lock the standard and maintain color repeatability in production.
In practice:
-
Sample approval first: we confirm color, gloss, texture, and front/back appearance as applicable.
-
Controlled production: we run the same coating material and process to minimize batch-to-batch variation.
-
We support matte, satin, and gloss finishes. For complex geometries, we’ll flag areas where appearance variation is more likely (e.g., deep recesses or shadowed zones).
These functional surfaces must remain assembly-ready and electrically reliable:
-
Threaded holes: High-temperature plugs or thread protectors keep coating out so fasteners install properly.
-
Grounding / conductive contact areas: Either left uncoated through masking or thickness-limited to maintain conductivity.
-
Mating / locating surfaces: Masking is used to control build; we can also provide DFM input to reduce assembly risk.
For best results, please clearly mark on the drawing all areas that are no-coat, must remain conductive, or require thickness limits. We’ll propose the masking approach as part of the quotation.
Yes. If corrosion testing is required, SR MFG can support salt spray validation based on your specified standard, test duration, and acceptance criteria.
A typical report includes:
-
Sample details (material, coating/color, DFT, quantity)
-
Test standard and conditions (method used, duration, pass/fail criteria)
-
Test procedure and results (key photos and conclusions)
-
Lot/order traceability information (when requested)
Pinholes and blistering are often caused by outgassing (gas or volatiles released during curing), insufficient surface cleaning, or an unsuitable primer/system choice.
SR MFG countermeasures include:
-
Galvanized parts: Verify surface condition, ensure proper cleaning/activation, and select a compatible primer system.
-
Castings: Porosity can release gas during cure—when risk is high, we use more robust primers or sealing approaches.
A pre-bake/outgas bake is strongly recommended (and sometimes required) when:
-
The substrate is prone to outgassing (galvanized, cast, welded structures, enclosed cavities).
-
Similar parts have shown pinholes/blistering in past runs—pre-bake helps drive off volatiles and reduce recurrence.
Deep corners, narrow gaps, and hidden recesses are inherently harder to coat evenly. SR MFG typically addresses this by:
-
Optimizing racking and spray path: Adjusting hang orientation, gun angles, and spray sequence for more uniform coverage.
-
DFM recommendations: Suggesting small design changes when features are too deep or narrow to coat consistently.
-
Defining Class A surfaces up front: Aligning on which visible areas require the highest cosmetic control.
Rework is possible, but it follows clear standards. Minor defects may be repaired locally; for larger rework, we evaluate the risk of mismatched color/gloss and may re-confirm the approved sample if needed.
Our goal is that parts arrive ready to use out of the box. Common protections include:
-
Surface isolation: Protective film, individual bagging, or layer separators to prevent rubbing.
-
Shock protection: Corner guards, custom dividers, or locating trays to reduce movement in transit.
-
Packaging matched to cosmetic requirements: Higher cosmetic requirements typically need higher protection (and we’ll confirm the cost impact with you up front).
Pricing and lead time depend on factors such as number of colors, coating system, cosmetic standards, fixture/racking needs, and masking complexity.
In general:
-
MOQ: Depends on color count, fixture cost, and changeover requirements (multi-color programs may run in batches).
-
Color changeover: Depends on changeover frequency, cleaning requirements, and booth scheduling (rules can be defined per project).
-
Lead time: Different for prototyping vs. production; affected by pretreatment/masking complexity and inspection/testing needs (salt spray testing adds time).
For the most accurate quote, please provide drawings, color standard, quantities, and any required test standards—so we can clearly define MOQ, changeover rules, and lead time.
Metal Spray Painting Technical Resources
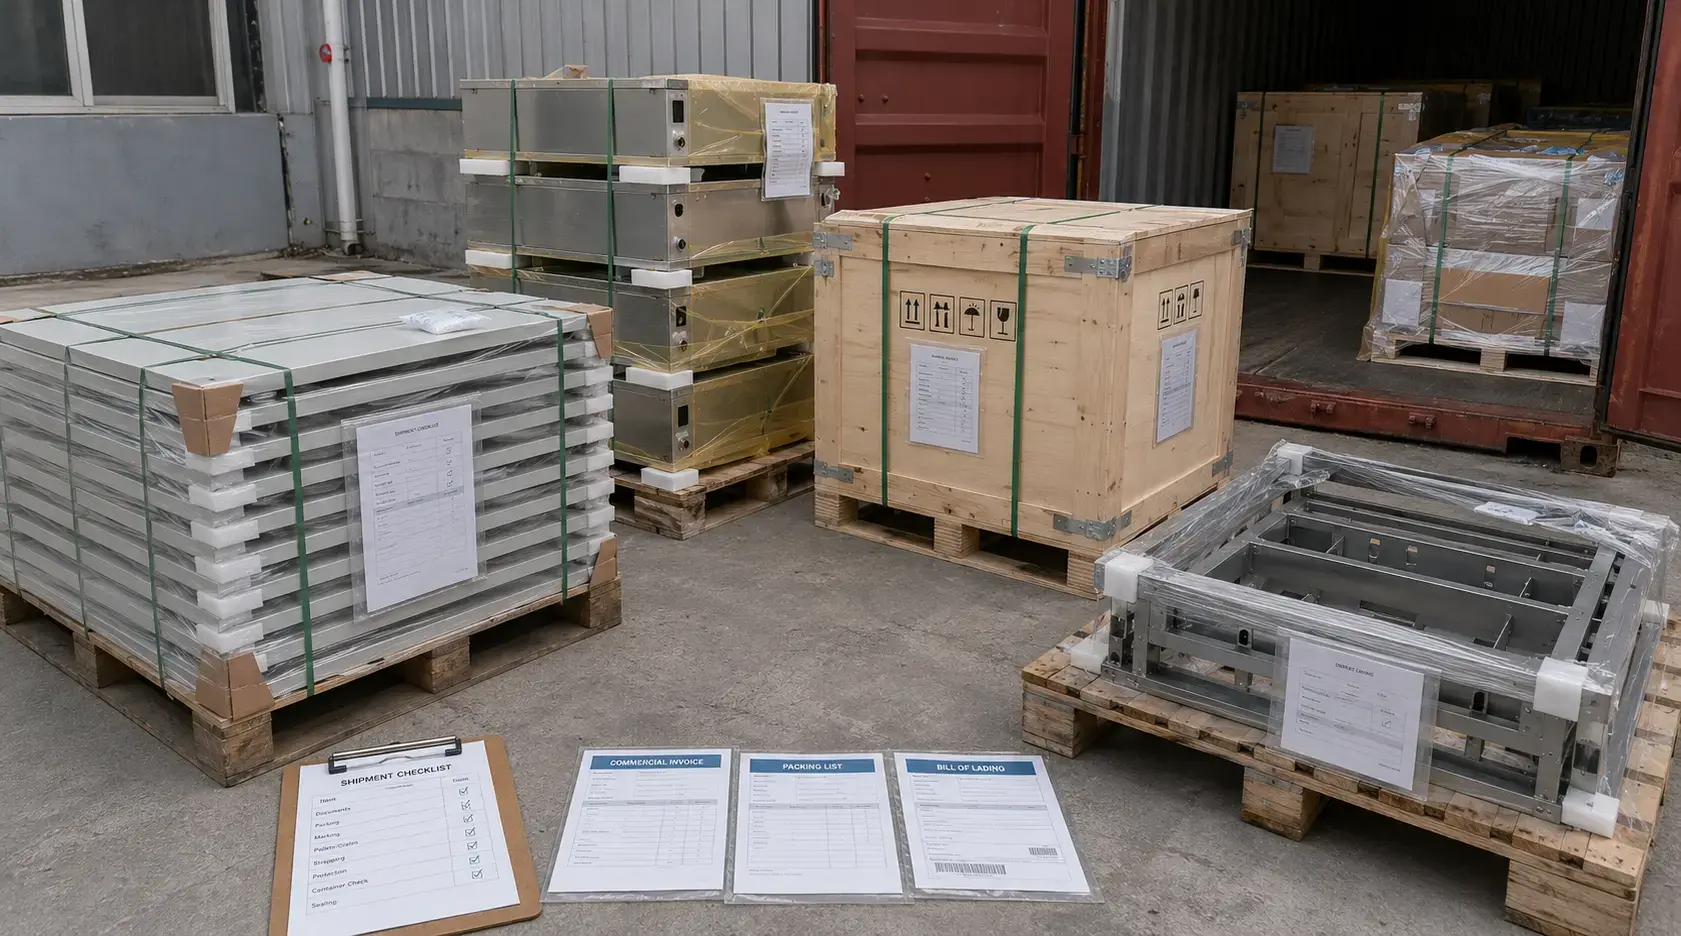
Sheet Metal Export Shipping Checklist from China: 6 Checks Before the Container Leaves
双瑞2026-09-12T02:39:19+00:008月 27, 2026|
The factory has confirmed your sheet metal parts are ready. Your freight forwarder is asking for the commercial [...]
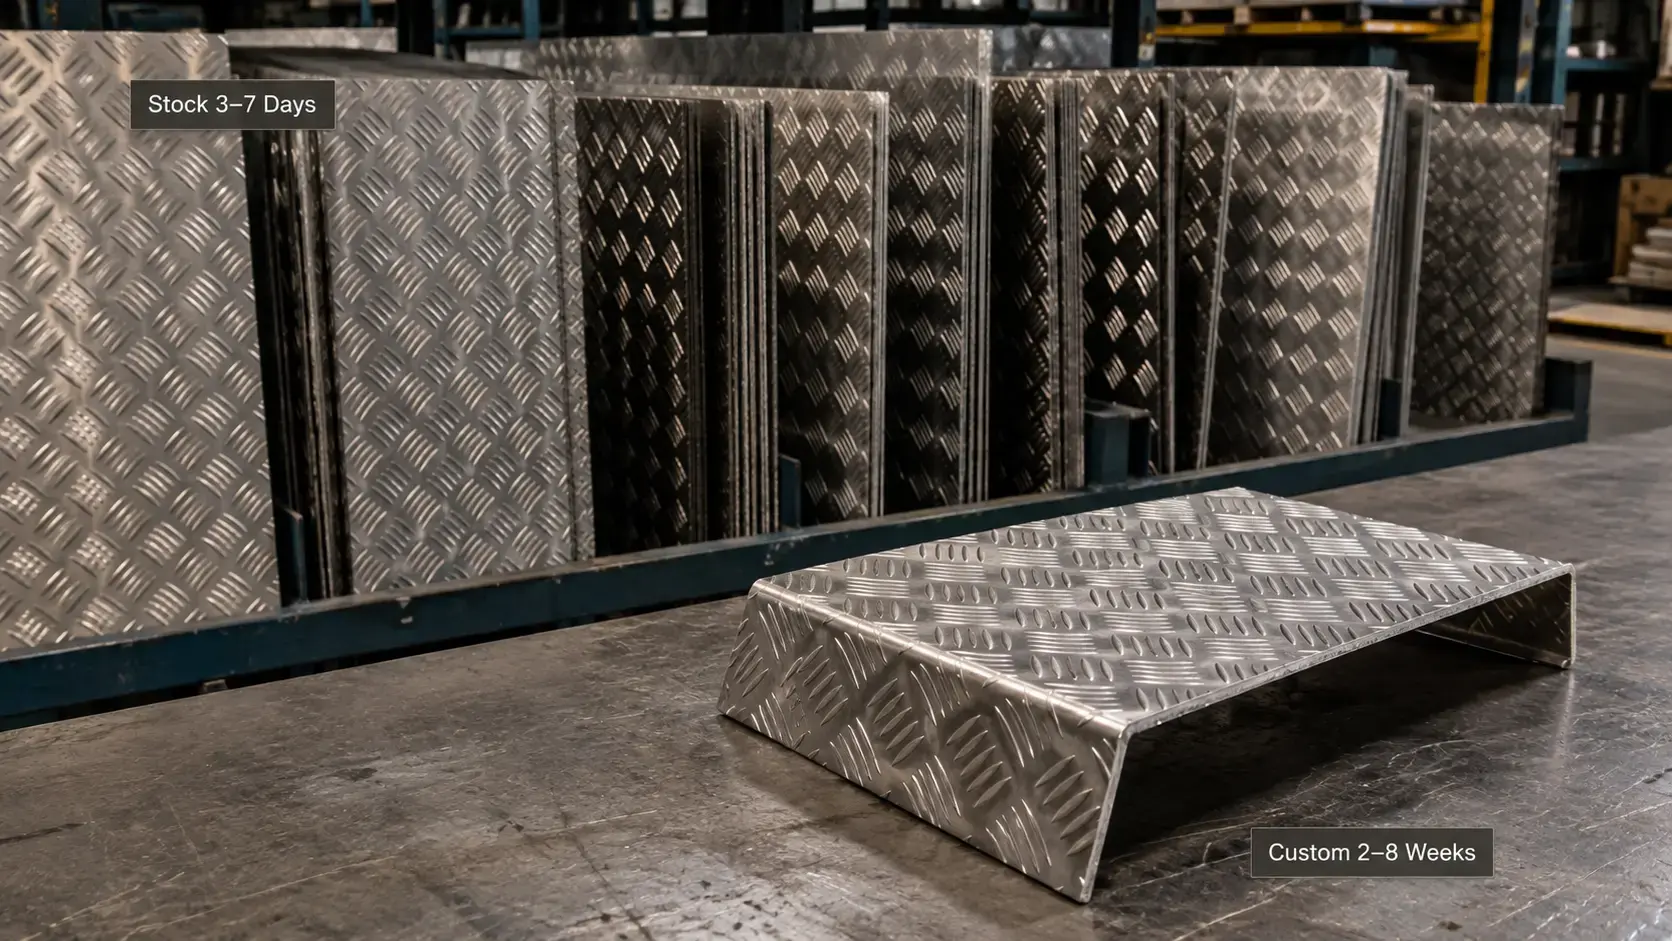
Checker Plate Lead Time & Availability: Stock, Mill Orders, and Fabrication Timelines
双瑞2026-09-12T05:44:40+00:009月 2, 2026|
Ordering checker plate looks like one of the easier procurement tasks in a fabrication project: pick a material, [...]
